
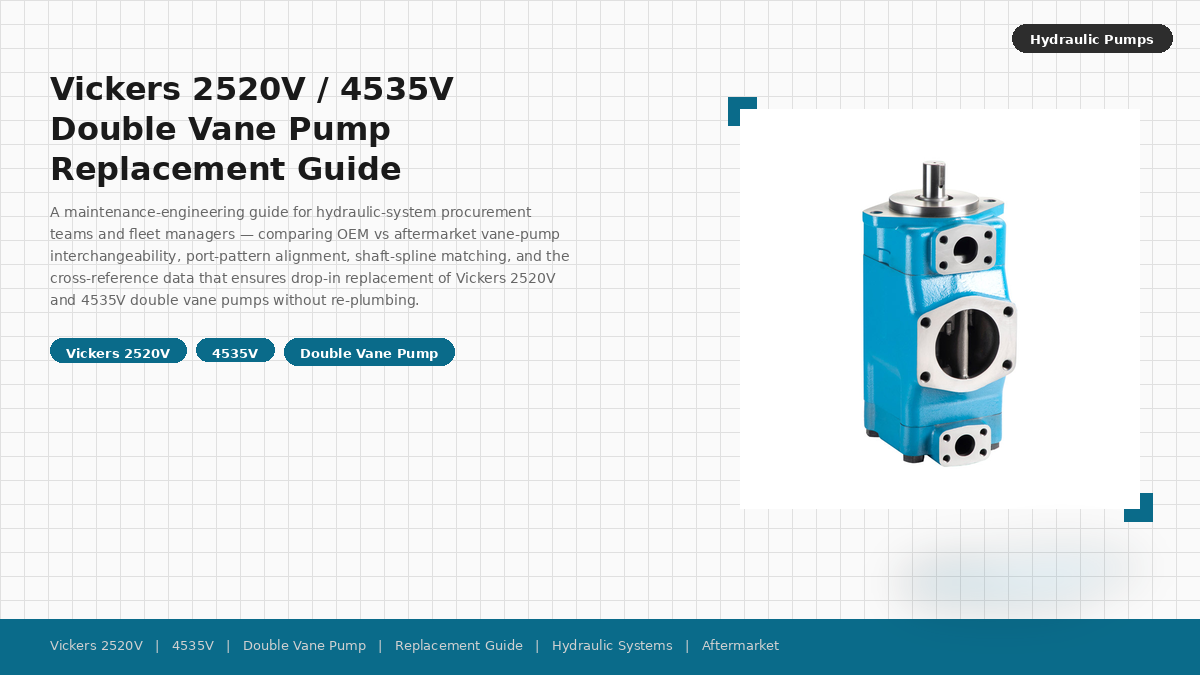
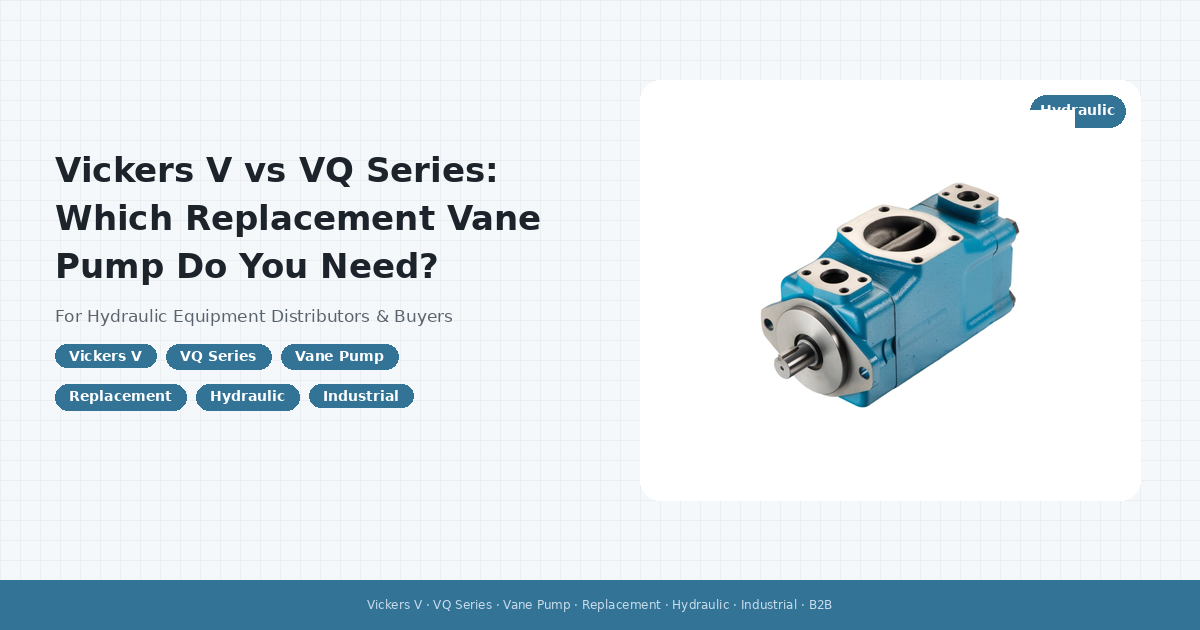
Denison T6-T7 Vane Pump Cartridge Procurement Documentation: What Heavy-Equipment Maintenance Teams Must Require from Hydraulic Component Suppliers
A comprehensive procurement documentation protocol for Denison T6-T7 series vane pump replacement cartridges. Covers material certification requirements per ISO 10468, dimensional verification against OEM specifications, performance testing standards, supplier qualification criteria, and the five-document package that separates professional-grade cartridge suppliers from commodity parts distributors offering undocumented replacements.
TL;DR
- The difference between a USD 200 cartridge and a USD 600 cartridge is documentation, not machining — material certifications, dimensional inspection reports, and performance test data that the supplier provides proactively, not upon request, separate a professional pump cartridge supplier from a commodity parts distributor.
- Denison T6-T7 cartridges operate at 240-300 bar continuous pressure with vane tip velocities exceeding 12 m/s — material substitutions without documented equivalent properties produce catastrophic failures within 500-2,000 operating hours that dimensional inspection alone cannot predict.
- A complete procurement documentation package should include five documents: material certification to ISO 10468, dimensional inspection report, performance test curve at rated pressure and speed, surface finish measurement report, and supplier ISO 9001 certificate with scope explicitly covering hydraulic pump components.
The Documentation Gap That Separates Professional Suppliers from Parts Distributors
When a hydraulic maintenance team orders a replacement Denison T6 or T7 vane pump cartridge, they are not ordering a machined metal assembly — they are ordering a performance guarantee. The cartridge must deliver the specified flow rate at the specified pressure within the specified volumetric efficiency tolerance for the specified service life, typically 8,000-12,000 operating hours in a properly maintained hydraulic system. If the cartridge fails prematurely due to vane breakage, cam ring wear, or excessive internal leakage, the cost is not limited to the replacement cartridge. The cost includes the machine downtime at USD 500-5,000 per hour for heavy equipment in mining, construction, or industrial processing, the labor to replace the failed cartridge at 4-8 hours and USD 75-150 per hour, the hydraulic oil contaminated by the failure debris that must be drained and filtered or replaced, and the potential for secondary damage to downstream hydraulic components including valves, cylinders, and motors that ingested metal particles from the failed cartridge.
The fully loaded cost of a single cartridge failure easily exceeds USD 5,000-25,000 depending on the equipment type and the extent of secondary damage. Against this cost, the difference between a USD 200 undocumented cartridge and a USD 600 fully documented cartridge — a USD 400 procurement saving — represents less than 2-8% of the cost of a single failure event. The economic logic is unambiguous: the documentation that verifies the cartridge was manufactured to specification is worth far more than the purchase price difference. According to ISO 10468, the international standard for hydraulic fluid power components, documentation requirements are an integral part of the procurement specification, not an optional addendum. Yet procurement teams routinely select the lowest-bid supplier and discover the documentation gap only when a failure occurs and the root cause analysis reveals that the cartridge material did not meet the OEM specification.
Material Certification: The First Line of Defense Against Premature Failure
The Denison T6 and T7 vane pump cartridges operate under conditions that push hydraulic component materials to their engineering limits. The cam ring — the kidney-shaped internal profile against which the vanes slide — experiences contact stresses of 500-800 MPa at the vane tip interface. The vanes themselves are subject to alternating bending stresses as they extend and retract during each revolution, cycling from minimum to maximum stress 24-30 times per second at 1,450-1,800 RPM pump speed. The rotor end faces experience sliding contact against the pressure plates with a thin hydrodynamic oil film that locally reaches temperatures of 120-150°C at the high-pressure port edge where the oil has just been compressed from suction to discharge pressure.
Under these conditions, material substitutions that would be acceptable in lower-stress hydraulic components produce failures that a dimensional inspection cannot predict. A cam ring manufactured from AISI 52100 bearing steel has a rolling contact fatigue life of approximately 10^8 cycles at the design contact stress. A cam ring manufactured from AISI 4140 alloy steel — substituted by a cost-reducing supplier — has a fatigue life of approximately 10^6-10^7 cycles at the same stress level, one to two orders of magnitude shorter. The parts are dimensionally interchangeable and would pass a standard incoming dimensional inspection. But the substituted cam ring will fail at 500-2,000 hours instead of 8,000-12,000 hours, and the failure will be attributed to a generic manufacturing defect with no obvious dimensional cause, making root cause analysis impossible without destructive metallurgical testing.
The VICKS T6-T7 cartridge documentation package includes material certifications that identify the specific material grade and heat treatment condition for every load-bearing component: cam ring (steel grade, hardness, case depth if surface-hardened), vanes (steel grade, hardness, surface coating if applicable), rotor (steel grade, hardness), pressure plates (bronze or steel grade, hardness), and sealing elements (elastomer grade, temperature rating, fluid compatibility). Each material certification is traceable to a specific heat number from the material supplier and includes the chemical composition analysis and mechanical property test results for that heat. This traceability means that if a material-related failure does occur, the root cause analysis can trace the failed component back to the specific material lot and determine whether the failure was due to material non-conformance, manufacturing defect, or application conditions beyond the component's design limits.
Dimensional Verification: Beyond Go/No-Go Gauging
A vane pump cartridge contains approximately 8-15 critical dimensions that determine its performance: the cam ring profile which controls the vane displacement and the pump's theoretical displacement per revolution, the vane slot width and depth in the rotor which controls vane clearance and the risk of vane sticking or vane flutter, the rotor end-face flatness and parallelism which controls the end clearance and volumetric efficiency, and the clearance between the rotor OD and the cam ring ID which controls internal leakage between the high-pressure and low-pressure zones. A go/no-go gauge can verify that these dimensions fall within the specified tolerance band, but it cannot tell the maintenance team where within that band the actual dimension falls — and for hydraulic pump performance, the difference between "barely within tolerance" and "nominal" can be significant, particularly for volumetric efficiency at high pressure.
A complete dimensional inspection report provides the measured value for each critical dimension, not just a pass/fail indication. This allows the maintenance team to compare the measured values against the OEM specification and identify any dimensions that are within the tolerance band but trending toward the limit, to trend dimensional data across multiple cartridge purchases to detect supplier process drift before it produces out-of-tolerance parts, and to correlate dimensional data with field performance — if cartridges with rotor end-face flatness at the upper tolerance limit consistently show 2-3% lower volumetric efficiency than cartridges at nominal flatness, the maintenance team can tighten the incoming inspection criterion without waiting for out-of-tolerance parts to arrive. Our VQ series cartridge program for Eaton Vickers pumps and Rexroth A4VSO piston pump cartridges provide the same documentation standard across both Denison and Vickers platforms for maintenance teams managing mixed equipment fleets.
Performance Testing: What Dimensional Data Cannot Verify
The ultimate verification of a replacement vane pump cartridge is not dimensional inspection but performance testing: does the assembled cartridge deliver the specified flow rate at the specified pressure with the specified volumetric efficiency? A cartridge with all critical dimensions within tolerance can still underperform if the interactions between components — vane clearance in the rotor slots, cam ring surface finish, pressure plate flatness — combine to produce higher internal leakage than the design predicts. Performance testing on a calibrated hydraulic test stand verifies the cartridge's actual output against its rated specifications and provides the objective evidence that the maintenance team needs to confidently install the cartridge and return the machine to service.
A complete performance test report should include: flow rate vs. pressure curve at the rated pump speed (typically 1,500 or 1,800 RPM) showing the flow at minimum pressure (0-10 bar), at the rated continuous pressure (240-300 bar for T6-T7 series), and at two intermediate pressure points; volumetric efficiency calculated as the ratio of actual flow to theoretical flow at each pressure point — a cartridge in good condition should show efficiency above 92% at rated pressure; a note of any unusual noise, vibration, or pressure pulsation observed during the test; and the test fluid viscosity and temperature, since volumetric efficiency is temperature-dependent. The Vickers V/VQ vane pump and Yuken PV2R series test protocols follow the same standardized procedure applied across our entire vane pump product line, ensuring consistent performance documentation regardless of the pump platform.
The Five-Document Procurement Package: A Template for Maintenance Teams
Based on 30 years of hydraulic component specification and field troubleshooting, I recommend that heavy-equipment maintenance teams require the following five documents as a standard procurement package for every replacement pump cartridge order. These documents should be provided by the supplier proactively — before shipment, not after a failure — and should be maintained in the equipment's maintenance records for the service life of the cartridge.
Document 1: Material Certification per ISO 10468 or EN 10204 Type 3.1, identifying the material grade, heat treatment condition, and mechanical properties (hardness, tensile strength, yield strength) for the cam ring, vanes, rotor, and pressure plates. Must include heat number traceability to the material supplier's mill test certificate. Document 2: Dimensional Inspection Report with measured values for all critical dimensions: cam ring profile, vane dimensions (length, width, thickness), rotor slot widths, rotor end-face flatness and parallelism, pressure plate flatness, and overall assembly dimensions. Measurement equipment identification and calibration status should be noted. Document 3: Performance Test Report with flow vs. pressure curve, volumetric efficiency at rated pressure, test fluid specification and temperature, and any observations of noise, vibration, or pulsation during the test. Document 4: Surface Finish Report with roughness (Ra) measurements for the cam ring internal surface, vane sliding surfaces, rotor end faces, and pressure plate running surfaces — surface finish directly affects the hydrodynamic oil film that separates sliding surfaces, and roughness 50% higher than specification can reduce the oil film thickness below the critical value and initiate metal-to-metal contact. Document 5: Supplier Quality System Certificate with current ISO 9001 certificate with a scope explicitly covering design and manufacture of hydraulic pump components.
Frequently Asked Questions
How can maintenance teams verify that a material certification is authentic and not fabricated?
Verify the certification laboratory's ISO/IEC 17025 accreditation status on the national accreditation body's website — for example, A2LA in the United States, UKAS in the United Kingdom, or CNAS in China. The accreditation certificate number on the material test report should match the laboratory's current accreditation listing. Additionally, verify that the heat number on the material certification matches a physical marking on the component — the cam ring, rotor, or vanes should have the heat number laser-etched or stamped on a non-wear surface. If the supplier cannot provide heat number traceability to a physical marking on the component, the material certification chain is broken and the certification document has no evidentiary value. Contact the material supplier identified on the certification directly to verify that the heat number exists in their production records and that the chemical composition and mechanical property data match their records for that heat.
What is the typical lead time for a documented Denison T6-T7 cartridge versus an undocumented one?
Undocumented cartridges from commodity distributors are typically available from stock with 1-3 day delivery — the distributor stocks cartridges based on part number cross-reference without providing any documentation beyond a commercial invoice. Documented cartridges from professional suppliers typically ship within 5-10 business days because the supplier assembles the documentation package for each order: pulling the material certifications from the raw material receiving records for the specific heat numbers used in that production batch, generating the dimensional inspection report from the in-process and final inspection measurements, and including the performance test report from the production test stand. Rush orders can ship within 2-3 business days with the documentation package following by email. Our ABT servo vane pumps and M4C hydraulic vane motors follow the same documentation lead time protocol.
What is the expected volumetric efficiency difference between a genuine OEM cartridge and a quality aftermarket replacement?
A quality aftermarket cartridge manufactured to the OEM material and dimensional specifications should deliver volumetric efficiency within 2-4% of the OEM cartridge at rated pressure when new. The primary determinants of volumetric efficiency are the end clearance between the rotor faces and the pressure plates, which is controlled by the rotor and pressure plate flatness and the assembly procedure, and the radial clearance between the rotor OD and the cam ring ID. Aftermarket cartridges that meet the same flatness tolerance and clearance specification as the OEM will deliver comparable volumetric efficiency. Cartridges with looser clearances — sometimes specified intentionally by aftermarket manufacturers who prioritize tolerance for contaminated oil over peak efficiency — may show 4-8% lower volumetric efficiency, which translates to 4-8% lower flow at rated pressure and correspondingly slower hydraulic actuator speeds. This is a design trade-off that should be disclosed by the supplier and evaluated by the maintenance team against the equipment's performance requirements. For applications where hydraulic cycle time is a critical production metric, even a 3% flow reduction may be unacceptable; for applications with significant duty cycle margin, the looser-clearance cartridge may be an acceptable cost-value trade-off when accompanied by full documentation.