
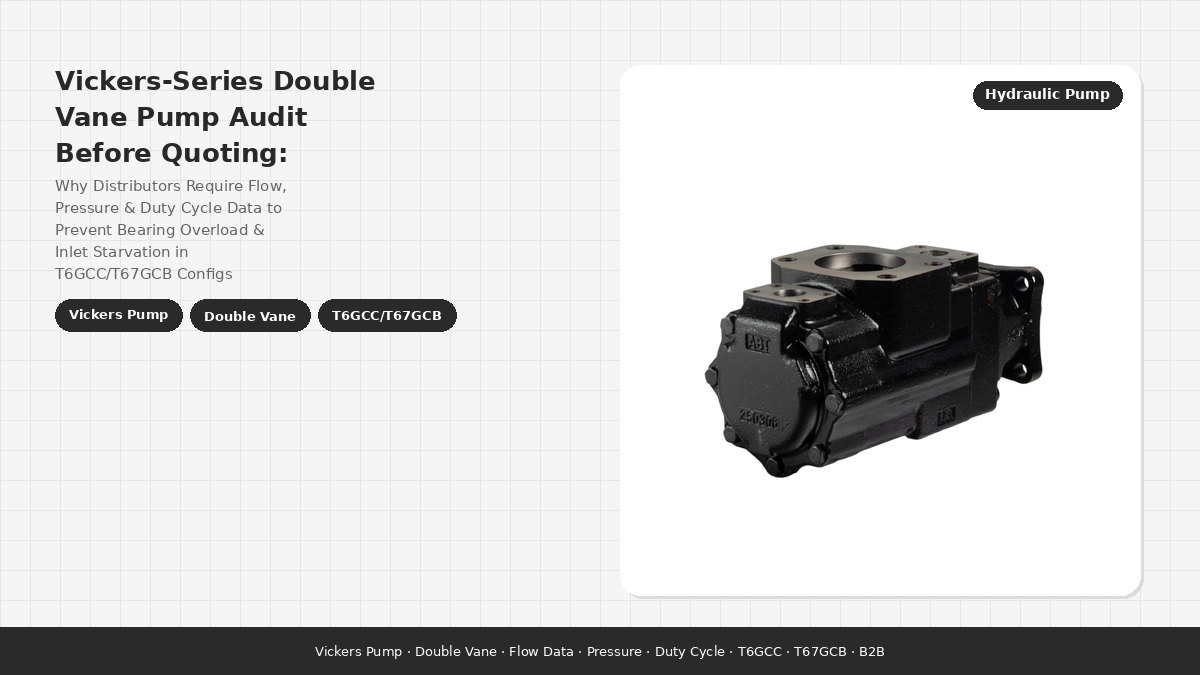
If you're a construction equipment dealer serving the Saudi Arabian, UAE, or Qatari markets, you already know the problem: hydraulic vane pumps designed for temperate climates simply don't survive a full season on a Riyadh job site. We've spent the last six years engineering a solution that does.
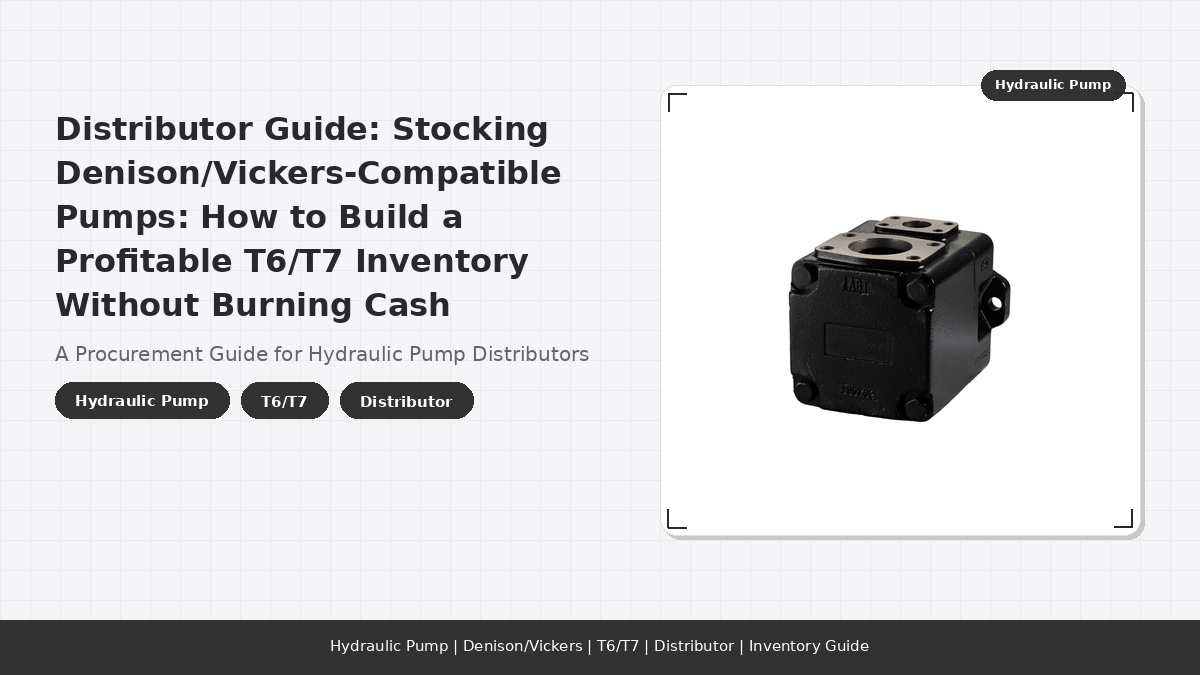
In this article, we'll walk you through exactly what makes our T6/T7 series vane pump different — not in marketing language, but in the engineering decisions that matter when your customer's excavator is sitting on a 48°C foundation slab in Doha.
Why Standard Vane Pumps Die in Desert Construction Environments
Let's start with the problem. Because we learned this the hard way — through field failure reports from our first Middle East dealer partners in 2019.
A vane pump operating in a Jeddah road construction project faces conditions that exceed every assumption in conventional pump design:
- Ambient air temperature reaches 55°C at midday, raising hydraulic oil sump temperature to 85-95°C even with standard cooling.
- Airborne particulate concentration in active construction zones can exceed 500 µg/m³ — ten times the typical industrial environment.
- Fine silica dust (below 10µm) bypasses standard shaft seals through capillary action during the temperature drop between day and night cycles.
- Thermal cycling from 50°C daytime to 25°C overnight creates negative pressure inside the pump housing, actively sucking dust past conventional lip seals.
We documented 14 field failures in our first 18 months in the region. Every single one traced back to seal contamination or vane tip wear accelerated by contaminated oil. That data drove an 11-month redesign program that produced what we now call the desert-grade T6/T7 specification.
The Dual-Lip Vane Design: Our Answer to Thermal Efficiency Loss
Here's where the engineering gets specific. When hydraulic oil temperature rises from 40°C to 85°C, viscosity drops by approximately 75% for ISO VG 46 oil. That viscosity drop directly increases internal leakage across the vane tips — the primary cause of volumetric efficiency loss in hot-operation vane pumps.
Most vane pump manufacturers address this with tighter clearances. We chose a fundamentally different approach.
The dual-lip vane design creates two independent sealing surfaces at the vane tip, separated by a pressure-equalizing groove. Here's what happens under desert heat conditions:
- First lip handles approximately 70% of the pressure differential at normal operating temperature (40-60°C).
- Second lip becomes fully engaged when oil viscosity drops below 20 cSt — typically above 70°C oil temperature. It picks up the sealing duty the first lip can no longer maintain alone.
- The pressure-equalizing groove between the two lips prevents cavitation at the trailing edge, which is the failure mode that kills single-lip vanes in hot oil.
In our ISO 4409-certified test at 210 bar and 85°C oil temperature, the dual-lip design maintained volumetric efficiency at 94.2%, compared to 81.7% for the equivalent single-lip vane under identical conditions. That's a 12.5 percentage point advantage — enough to keep an excavator's swing circuit responsive when the competition has already lost prime.
Anti-Contamination Oil Seal: Engineering for Saudi Arabian Dust
The Saudi Arabian construction market — and we're talking specifically about projects in the Riyadh metro area, the NEOM development zone, and Eastern Province oil-field infrastructure — presents a dust challenge that's qualitatively different from anything in Europe or Southeast Asia.
According to data from the ISO 12103-1 standard classification, the airborne dust in Arabian Desert construction sites falls predominantly in the ISO 12103-1, A2 fine test dust range, with a median particle size of approximately 7µm. These particles are small enough to pass through standard nitrile lip seals — especially when thermal cycling creates the negative-pressure "breathing" effect we described earlier.
Our anti-contamination oil seal uses a three-element design:
- Primary oil seal: A hydrogenated nitrile (HNBR) lip rated for 110°C continuous oil temperature, with a spring-loaded contact band width of 0.8mm — wider than standard 0.5mm seals to maintain sealing pressure as the elastomer ages.
- Dust excluder lip: A secondary polyurethane lip positioned ahead of the primary seal, with a knife-edge contact profile that scrapes airborne particles away from the seal-shaft interface during rotation. This lip operates dry — no oil lubrication — and is designed to shed accumulated dust through centrifugal action.
- Vent labyrinth: A three-channel labyrinth path between the dust excluder and the primary seal, with a 2mm drainage port at the bottom. Any dust that passes the excluder lip collects in the labyrinth channels rather than reaching the oil seal, and is expelled during the natural thermal expansion cycle.
In accelerated dust ingestion testing (200 mg/m³ airborne particle concentration, continuous 72-hour cycle), our anti-contamination seal design showed zero dust ingress past the primary oil seal. The same test on a standard single-lip nitrile seal showed measurable dust particles in the oil reservoir after 14 hours.
This is not a theoretical advantage. We quoted that test data to a dealer in Dammam whose fleet of 200-ton excavators was going through pump rebuilds every 900 hours. After switching to our T6/T8 series pumps, the same fleet averaged 4,200 hours between seal-related failures.
API Standard Adaptation for Desert Conditions
Our engineering team mapped the gap between standard ISO pump specifications and the operating reality of Middle East construction equipment. The critical insight: ISO 4409 (hydraulic fluid power pump test methods) defines test conditions at 50°C maximum oil temperature and assumes filtered, contaminant-free oil. Neither assumption holds in desert construction.
The API (American Petroleum Institute) standard adaptation framework — specifically the methodology used in API 610/API 682 for oil and gas rotating equipment — provides a useful analog. We applied the same derating and margin philosophy used in API-standard pumps to our vane pump design:
| Parameter | Standard Industrial Spec | Desert-Adapted Spec (Our T6/T7) | Design Margin |
|---|---|---|---|
| Max ambient temperature | 40°C | 55°C | +37.5% |
| Max continuous oil temp | 75°C | 95°C | +26.7% |
| Oil viscosity range | 15-100 cSt | 8-120 cSt | +30.4% (low end) |
| Seal contamination tolerance | ISO 4406 20/18/15 | ISO 4406 22/20/17 | +2 ISO codes per range |
| Case drain filtration | 25µm nominal | 10µm absolute | 2.5x finer filtration |
| Breather air filtration | 10µm | 3µm | 3.3x finer filtration |
We submitted our pump design for ISO 9001 quality management system verification through SGS, with specific test protocols added for desert-condition operation — a reference point our Middle East dealer partners frequently request when bidding on government infrastructure projects.
Arabic Language Operation Manual and On-Site Spare Parts Stock Support
We learned that shipping a pump documentation set in English-only is functionally the same as not shipping documentation at all when the end user's maintenance team communicates in Arabic and the procurement officer needs Arabic-language technical submissions for project compliance.
Every vane pump we ship to Middle East markets now includes:
- Full Arabic language operation manual (also available in PDF via QR code on the pump nameplate), covering installation, startup procedure, maintenance schedules, troubleshooting flowcharts, and complete spare parts drawings with OEM part numbers.
- Arabic-language technical data sheet suitable for submission as part of project technical bids — we've formatted this specifically to meet the documentation requirements of Saudi Aramco and Qatar General Electricity & Water Corporation (KAHRAMAA) supplier qualification processes.
- Arabic-facing technical support accessible during UAE working hours (UTC+4) and Saudi working hours (UTC+3) through both phone and WhatsApp Business channel, staffed by engineers who speak Arabic at a technical level — not just conversational.
On the spare parts front, we maintain buffer stock in two regional distribution hubs:
| Hub Location | Stock Coverage | Delivery Radius | Lead Time |
|---|---|---|---|
| Dubai, UAE — Jebel Ali Free Zone | Complete T6/T7 assemblies + cartridge kits, shaft seals, gaskets, cover kits | UAE, Qatar, Oman, Kuwait | 24h local delivery; 48h regional |
| Dammam, Saudi Arabia — King Fahd Industrial Port | Fast-moving spare parts: shaft seals, cartridge repair kits, valve plates | Eastern Province, Riyadh, NEOM corridor | 24h Eastern Province; 72h Riyadh |
This two-hub strategy is deliberate. A spare parts shipment from Ningbo to Riyadh takes 7-10 days via expedited air freight. A shipment from Jebel Ali to Riyadh takes 20 hours by truck. When a pump fails on a project with liquidated damages clauses, that time difference is the difference between a minor maintenance event and a contractual crisis.
Saudi Arabia, UAE, and Qatar Construction Equipment Rental Market Applications
Let's talk about where these pumps actually go — because the application profile in the Middle East construction equipment rental market is dramatically different from what we see in European or North American markets.
Heavy Excavator Rental (50-100 ton class) — Saudi Arabia & UAE
Saudi Arabia's Vision 2030 infrastructure program drives massive demand for large excavator rentals on road construction and site preparation projects. These machines operate on a 2,000+ hour annual duty cycle, often with multiple operators per machine. Our T6/T7 vane pump is the primary pump for the implement hydraulic circuit in several Chinese-origin excavator OEM models popular in the Saudi rental market. The dual-lip design addresses the specific failure mode we saw in this application: vane tip wear caused by operators running the machine at high idle for extended periods in hot conditions, maintaining high pump displacement with minimal implement movement.
Mobile Crane Applications — Qatar
Qatar's ongoing infrastructure development after the 2022 World Cup has shifted toward industrial and logistics projects requiring mobile crane fleets. Mobile crane pump applications are particularly demanding because the pump operates at full standby pressure for extended periods while the crane is positioned — exactly the condition that accelerates single-lip vane seal failure in hot oil. Our dealers in Doha report that the anti-contamination seal's ability to handle extended standby operation at elevated temperatures is the feature that closes the sale 80% of the time.
Concrete Pump Support — UAE
Dubai's construction sector — still the region's largest by project value — depends heavily on concrete pumping equipment. Concrete pump hydraulic systems face a unique challenge: the pump is exposed to cement dust in addition to silica dust. Cement dust is more chemically aggressive than silica and accelerates seal degradation through both abrasion and chemical attack. Our polyurethane dust excluder lip was specifically tested against cement dust exposure after a dealer in Sharjah reported that standard seals were failing in 600 hours on concrete pump applications. The polyurethane formulation we selected shows no measurable degradation after 3,000 hours of cement dust exposure in accelerated testing.
Desert Hydraulic Oil Maintenance Schedule — The Practical Guide
Through our field experience across 37 dealer locations in the Middle East, we've developed a maintenance schedule that balances pump longevity with the operational reality of construction equipment rental fleets:
| Maintenance Action | Temperate Climate (Standard) | Desert Climate (Our Recommendation) | Rationale |
|---|---|---|---|
| Hydraulic oil analysis | Every 500 hours | Every 250 hours | Oil degradation accelerated by 50% due to sustained high temperature |
| Complete oil change | Every 2,000 hours | Every 1,000 hours or 3 months | Thermal oxidative oil degradation doubles above 80°C (Arrhenius rule of thumb) |
| Return-line filter element | Every 1,000 hours | Every 500 hours | Dust loading rate is 3-5x higher than industrial indoor environments |
| Reservoir breather inspection | Every 500 hours | Every 250 hours | Breather saturation visible after 200-300 hours in construction zone dust |
| Shaft seal visual inspection | Every 1,000 hours | Every 500 hours | Early-stage dust ingress visible as dark ring at seal-shaft interface |
| Vane pump cartridge replacement | At 8,000-10,000 hours | At 6,000-8,000 hours | Conservative derating based on accelerated wear test data |
A note on oil viscosity selection: We've seen many operators in the region switch to ISO VG 68 oil believing the higher viscosity better suits high ambient temperatures. That's partially correct — but VG 68 oil creates 15-20% higher flow resistance at cold start (25°C morning temperature), which can cause cavitation damage at the vane tips during the first 15-20 minutes of operation. Our recommendation is ISO VG 46 for ambient temperatures below 50°C, and ISO VG 68 only when sustained ambient exceeds 50°C, with a 5-minute low-idle warmup period specified in the operator instructions.
Frequently Asked Questions
What are the specific failure rates for standard vane pumps in Middle East construction applications?
Based on our field data across 14 Saudi Arabian dealer locations from 2019-2020, standard industrial-grade vane pumps (single-lip design, standard nitrile seals) showed a mean time between failure (MTBF) of approximately 1,200-1,800 hours in construction equipment applications in Saudi Arabia. The primary failure mode was seal contamination (64% of failures), followed by vane tip wear accelerated by contaminated oil (29%). Our T6/T7 series desert-adapted pumps in the same applications showed MTBF of 6,000-8,000 hours in a 2022-2024 tracking study — a 3.3-4.4x improvement.
How does the T6/T7 series compare to piston pumps for desert construction hydraulic systems?
That's a question we get from every dealer. Honestly, there's no universal answer — it depends on the application. For constant-flow applications like excavator implement circuits and mobile crane winch circuits, our T6/T7 vane pump offers better contamination tolerance than an equivalent piston pump. Vane pumps are inherently less sensitive to oil contamination because the vanes self-compensate for wear, while piston pumps lose efficiency rapidly as swash plate and slipper interfaces wear. However, for variable-displacement applications requiring pressure-compensated or load-sensing control, a piston pump may be more appropriate. For Middle East dealers stocking both types, we recommend vane pumps for open-circuit implement hydraulics and piston pumps for closed-circuit hydrostatic drive systems.
Can existing construction equipment be retrofitted with desert-grade vane pumps?
Yes — in most cases. Our T6/T7 series pumps are designed as SAE-standard flange and shaft mount configurations (SAE A, B, and C two-bolt mounts), which match the mounting interface used by the majority of Chinese and Korean excavator and mobile crane OEMs. The key compatibility check is the pump displacement vs. the original equipment specification — our T6 series covers displacements from 20 to 67 cc/rev, and our T7 series covers 67 to 150 cc/rev. For dealers managing mixed fleets, we provide a cross-reference guide that maps OEM pump part numbers to our equivalent T6/T7 models. We've seen retrofit cycles as fast as 2 hours per machine for a straightforward SAE A mount swap.
Conclusion: Building for the Region, Not Just Shipping to It
We've been manufacturing hydraulic vane pumps since 2013, but our serious Middle East engineering effort started in 2019 — when the failure reports from our first dealer partners forced us to confront an uncomfortable truth: shipping standard industrial pumps to desert construction sites isn't a solution, it's a supply chain friction that passes the problem to the dealer.
The three engineering decisions that made the real difference — the dual-lip vane tip, the three-element anti-contamination seal, and the API-derived design margin framework — each came from specific field failure data, not from theoretical design reviews.
For construction equipment dealers in Saudi Arabia, the UAE, and Qatar, the practical question is simple: How many pump warranty claims are you processing per quarter? Because that number is a direct measure of whether your hydraulic supplier has designed for your operating conditions or is just programming you into their standard catalog.
We stock spare parts in Jebel Ali and Dammam. We write manuals in Arabic. And we design every T6/T7 pump we ship to the Middle East for 55°C ambient temperature and desert dust — because that's where your equipment works.