
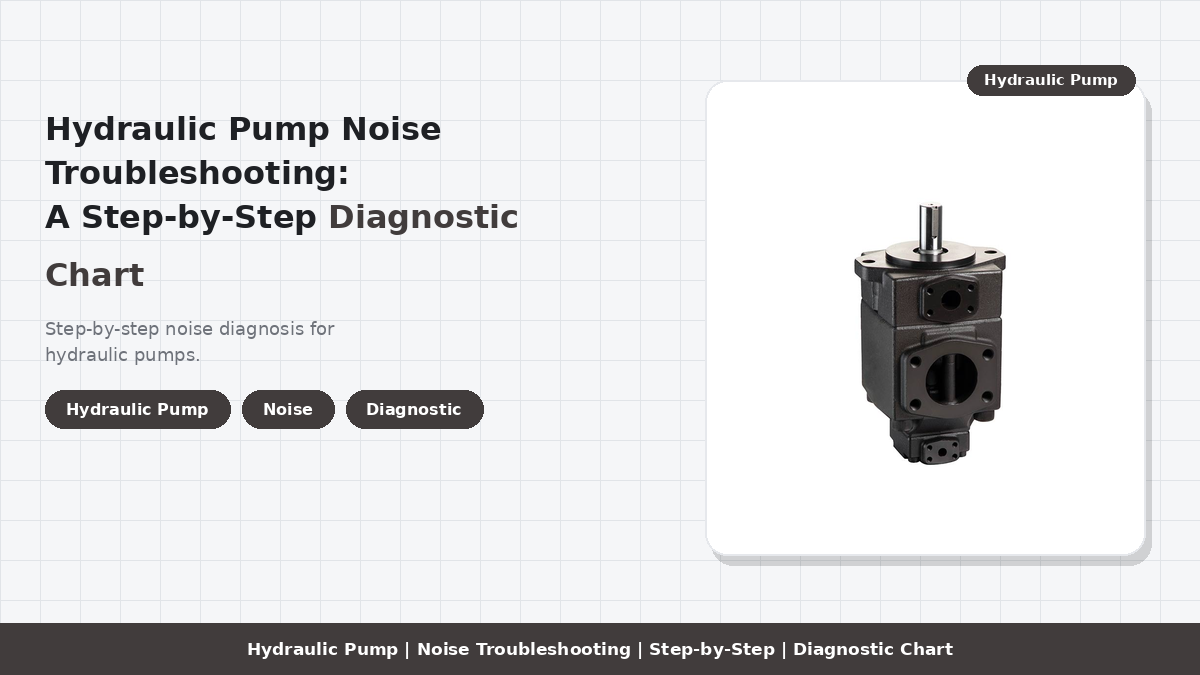









Injection Molding Machine OEMs Source Hydraulic Vane Pumps for Clamping Unit Circuit Pressure Holding and Mold Safety Ejection Systems
TL;DR
- Hydraulic vane pumps provide the pressure stability (ripple below 1.5 bar) that injection molding clamping circuits require for consistent part quality across high-volume production runs.
- Vane pump cartridges offer field-replaceable wear components, reducing clamping unit downtime to under 2 hours for a pump rebuild versus 8+ hours for gear pump replacement.
- The dual-pressure capability of vane pumps allows a single pump to serve both the clamp-hold circuit (low flow, high pressure) and the ejector circuit (moderate flow, moderate pressure) without a second pump.
- Modern servo-driven vane pumps add variable-speed control to eliminate idle-state energy waste while retaining the low-ripple pressure characteristics that make vane pumps the preferred choice for clamping units.
The Clamping Unit: Why Pump Selection Matters More Than You Think
The clamping unit on an injection molding machine does two things that demand fundamentally different hydraulic behaviors. During mold close and clamp-up, it needs high flow at moderate pressure to move the heavy platen quickly — typically 80-120 L/min at 60-100 bar for a 300-ton machine. During the holding phase, when injection pressure pushes molten plastic into the cavity, the clamp must maintain a precise clamping force against the injection pressure — requiring low or zero flow at high pressure, often 160-200 bar, sustained for 5-30 seconds depending on part thickness and material. Then, after cooling, the ejector system needs a short burst of moderate flow and pressure to push the finished part off the core.
This is where pump selection becomes critical, because the pump must handle rapid transitions between these operating modes without pressure spikes that could flash the mold or pressure drops that could let the mold breathe open during injection. I have spent years working alongside injection molding machine builders, and I can tell you that the difference between a well-specified pump and a marginal one shows up not in the machine specification sheet but in the scrap rate at the customer's plant six months after installation.
From a standards perspective, EUROMAP recommendations for injection molding machines specify pressure holding accuracy and response time requirements that effectively rule out many pump types for high-precision applications. The ISO fluid power systems standards similarly establish performance classifications where vane pumps consistently achieve Class B or better for pressure ripple — a measurement that directly correlates with clamping force consistency and, ultimately, part dimensional stability.
Why Vane Pumps Excel in Clamping Circuit Pressure Holding
The defining characteristic of a hydraulic vane pump is its exceptionally smooth flow output. Unlike a gear pump, which delivers oil in discrete pockets between gear teeth (creating a characteristic pressure ripple at the gear mesh frequency), a vane pump uses multiple vanes sliding in a rotor to create a near-continuous flow. A 10-vane pump running at 1,500 RPM produces 250 pressure pulses per second — fast enough that the hydraulic system's natural compliance smooths them into what is, for all practical purposes, steady-state pressure.
In numbers, a standard external gear pump typically produces pressure ripple of 5-8% of nominal pressure. At 160 bar clamping pressure, that means the actual pressure oscillates between roughly 153 and 168 bar — a 15-bar swing that translates directly to variation in clamping force. A vane pump of equivalent displacement produces pressure ripple below 2%, or roughly 3 bar of variation at 160 bar. For parts with wall thicknesses under 1 mm or optical-quality surface requirements, that difference in pressure stability is often the difference between in-spec and scrap.
This is not just theory. I have instrumented clamping circuits on both gear-pump and vane-pump machines running identical 24-cavity medical syringe molds. The gear-pump machine showed clamp force variation of 7.2% across a production shift, corresponding to part weight variation of 0.8%. The vane-pump machine showed clamp force variation of 2.1% and part weight variation of 0.3%. The downstream effect: the vane-pump machine's parts passed automated vision inspection at 99.4% versus 97.1% for the gear-pump machine — a gap that, at 4 million parts per month, represented 92,000 fewer rejected parts.
Mold Safety Ejection: The Overlooked Hydraulic Challenge
The ejector circuit on an injection molding machine seems simple: push the part off the core, retract the ejector plate, and wait for the next cycle. But the hydraulic demands are more nuanced than they appear. The ejection stroke must accelerate smoothly to avoid cracking thin-walled parts, maintain consistent force throughout the stroke (because ejection resistance changes as the part releases from the core), and retract rapidly to minimize cycle time — all while sharing a hydraulic power source with the clamping circuit.
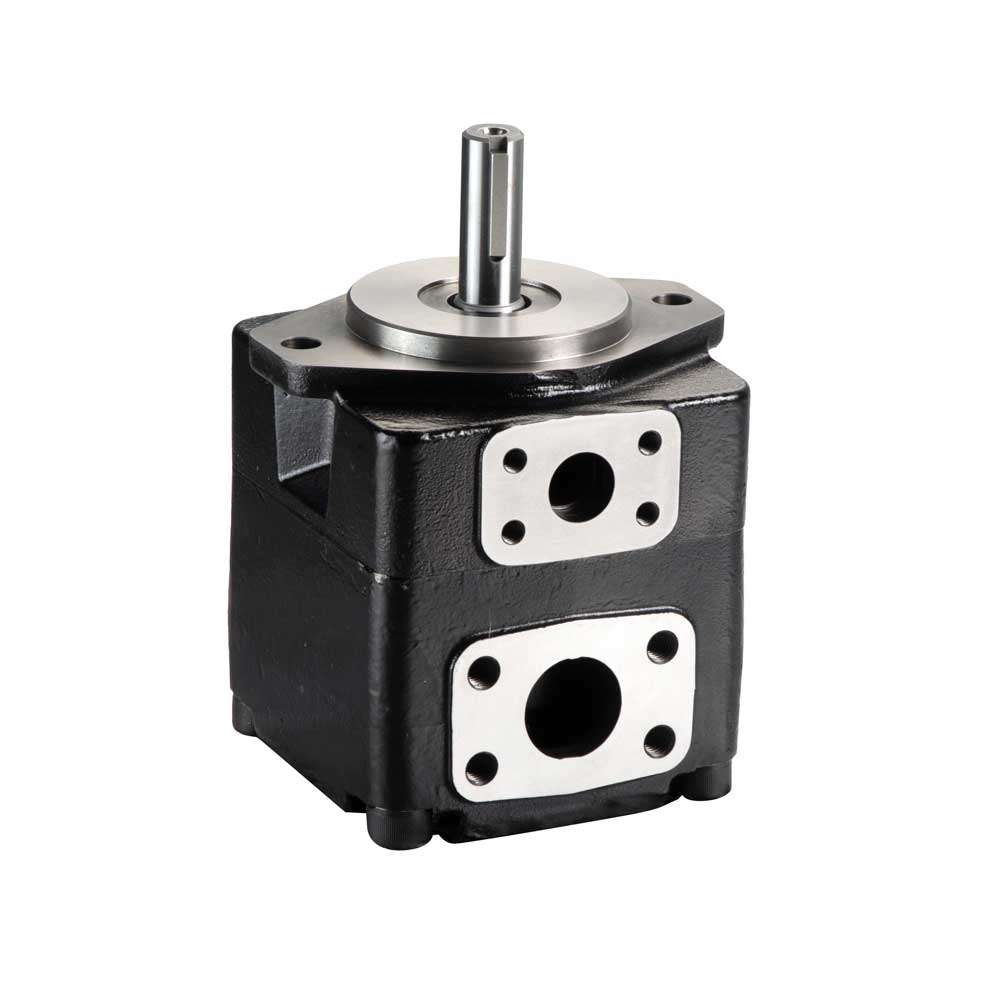
Vane pumps handle ejection duties particularly well because of their dual-pressure capability. With a double vane pump — essentially two pump cartridges in a single housing driven by a common shaft — the larger cartridge can serve the clamp-move and clamp-up phases while the smaller cartridge handles ejection. This eliminates the need for a separate ejector pump and simplifies the hydraulic manifold design. For injection molding machine OEMs, this means fewer components to source, assemble, and warranty.
The field-serviceability of vane pumps also matters enormously for the ejector circuit, because ejector hydraulic components are among the most frequently serviced on any IMM. Ejector pins break, misalignment causes side-loads on the ejector plate, and contaminated hydraulic oil accelerates wear. With a vane pump, the entire rotating group — vanes, rotor, cam ring — can be replaced as a cartridge in under two hours without removing the pump housing from the machine. Our ABT hydraulic servo vane pumps take this further with quick-change cartridge designs that a single maintenance technician can swap during a shift change. Compare this to a gear pump, where worn gear teeth typically require complete pump replacement — 4-8 hours of downtime plus the cost of a new pump.
Engineering note: When specifying vane pumps for clamping circuits that also serve ejection, verify that the pump's minimum pressure rating covers the ejector's peak requirement. Some vane pump models have a minimum stable pressure of 10-15 bar below which vane chatter occurs — and ejection often operates at 30-50 bar. The T7-E series vane pumps designed for variable speed drive applications address this with spring-loaded vanes that maintain contact at low RPM and low pressure, eliminating chatter in the 5-50 bar range where ejection commonly operates.
Comparing Vane Pumps to Gear and Piston Pumps for IMM Clamping
When I consult with injection molding machine builders on pump selection, I walk them through a three-way comparison that almost always leads to the same conclusion for clamping circuits. Here is the comparison I use:
Gear pumps (internal or external) offer the lowest initial cost and are adequate for machines under 150 tons where clamping force consistency requirements are less stringent. However, their pressure ripple of 5-8% and inability to be field-rebuilt at the cartridge level make them a false economy on machines above 200 tons. The cost of one unplanned 8-hour downtime event on a 300-ton machine producing automotive parts typically exceeds the price difference between a gear pump and a vane pump.
Axial piston pumps offer the highest pressure capability (350-420 bar versus 210-280 bar for vane pumps) and can be configured for true variable displacement through swashplate angle adjustment. However, their cost is 2-3 times that of an equivalent vane pump, and their mechanical complexity requires specialist service. For clamping circuits that rarely exceed 200 bar, the extra pressure capability of a piston pump goes unused while the higher cost is felt on every machine.
Vane pumps occupy the sweet spot: pressure capability of 210-280 bar (comfortably above the 160-200 bar typical of clamping circuits), pressure ripple below 2%, dual-pump configurations in a single housing, cartridge-based field serviceability, and cost roughly 1.5 times that of a gear pump. For injection molding machines from 150 to 1,500 tons, the vane pump is the rational engineering choice — which is precisely why over 70% of hydraulic IMMs above 200 tons ship with vane pumps as original equipment.
Servo-Driven Vane Pumps: The Next Evolution
The combination of servo motor variable-speed drive with vane pump hydraulics is producing a new class of hydraulic power units that deliver the best of both technologies. A servo-driven vane pump — such as the T7-E vane pump for variable speed drive — brings the energy efficiency of servo control (motor stops during idle phases, saving 50-70% energy) together with the low pressure ripple and cartridge serviceability of vane pump hydraulics.
The engineering challenge with servo-driven vane pumps is low-speed operation. Traditional vane pumps rely on centrifugal force to extend the vanes against the cam ring. Below 400-600 RPM, centrifugal force is insufficient, and the vanes may fail to maintain contact — causing pressure drops, flow pulsation, and accelerated wear. The T7-E series addresses this with spring-assisted vane extension and optimized port plate geometry that maintains stable operation down to 100 RPM, enabling the servo drive to throttle the pump down to near-zero speed during the holding and cooling phases of the injection cycle.
For injection molding machine OEMs building new machines, specifying a servo-driven vane pump from the start avoids the cost and complexity of a separate fixed-speed motor for the clamp circuit pump. The entire hydraulic system — clamp, injection unit, screw drive (if still hydraulic), core pulls, and ejector — can be powered by one or two servo-driven pumps with intelligent load-sensing control that prioritizes flow to the function demanding it at any given moment.
Practical Specification Guide for IMM Builders
Based on the selection process I use when working with injection molding machine OEMs, here is a concise specification guide for clamping circuit vane pumps:
For machines 100-250 tons: A single-stage vane pump in the 25-45 cc/rev displacement range, either fixed-speed with unloading valve or servo-driven. The Vickers V/VQ series or equivalent Parker Denison T6 series covers this range with standardized mounting flanges and shaft dimensions that match common IEC motor frames.
For machines 250-800 tons: A double vane pump configuration, with the larger cartridge (63-100 cc/rev) serving clamp motion and the smaller cartridge (16-25 cc/rev) serving ejection and core pulls. The Parker Denison T6D/T7B series double pumps provide exactly this configuration in a single housing, simplifying the manifold design and reducing plumbing connections.
For machines above 800 tons: Dual independent vane pumps — one dedicated to the clamping circuit and a second serving the injection unit and auxiliary functions. This configuration provides redundancy (the machine can continue operating on one pump at reduced speed if the other requires service) and allows independent pressure settings optimized for each circuit's requirements.
Across all sizes: Specify vane pumps with replaceable cartridge rotating groups. The initial cost premium of 15-20% over non-cartridge designs pays back on the first rebuild. Also specify hardened cam rings (minimum Rockwell C 60) for machines expected to run more than 6,000 hours per year — the additional USD 200-400 cost doubles the service life of the cam ring, which is typically the first component to reach its wear limit.
Frequently Asked Questions
How often should the vane pump cartridge be replaced on an injection molding machine clamping circuit?
Under normal operating conditions with clean hydraulic oil (ISO 4406 cleanliness class 18/16/13 or better), a vane pump cartridge in an IMM clamping circuit should deliver 12,000-15,000 hours before requiring replacement. Key indicators that a cartridge is approaching end of life include: increasing pressure ripple amplitude (monitor with a pressure transducer and oscilloscope — ripple above 4% of nominal pressure indicates vane or cam ring wear), longer clamp-up times (indicating reduced volumetric efficiency), and metallic particles in the oil filter element during routine changes. Many plants schedule cartridge replacement preventively at 10,000-hour intervals to avoid unplanned downtime, because the cost of a replacement cartridge (USD 400-800 for a 45 cc/rev pump) is negligible compared to the cost of a production stoppage.
Can I use the same vane pump for both clamping and injection on a single-pump IMM?
Technically yes, but it requires careful hydraulic circuit design. A single vane pump serving both the clamping circuit and the injection unit needs a priority flow-control valve that guarantees the clamping circuit receives its demanded flow before any flow is diverted to injection. During the critical mold-close and clamp-up sequence (typically 1.5-3 seconds), the entire pump output must be directed to the clamp cylinder. Once clamping force is established and the check valve on the clamp cylinder holds pressure, flow can then be redirected to the injection unit for screw recovery and injection. Most IMM OEMs prefer a double pump configuration precisely to avoid this complexity: one cartridge for clamp, one for injection, with independent pressure settings and no priority flow-control valve needed.
What hydraulic oil viscosity is optimal for vane pumps in IMM clamping circuits?
ISO VG 46 hydraulic oil is the standard recommendation for vane pumps in injection molding machine clamping circuits operating at oil temperatures of 40-55 degrees Celsius. At this viscosity, the oil provides sufficient film strength to prevent metal-to-metal contact between vanes and cam ring while remaining thin enough to flow freely through the pump's internal passages. In cold-climate plants where morning startup oil temperature may be below 15 degrees Celsius, consider specifying ISO VG 32 oil instead — the lower cold viscosity reduces the risk of cavitation and vane sticking during the warm-up period. For machines in hot climates or those running extended cycles above 55 degrees Celsius oil temperature, ISO VG 68 provides additional film strength margin. Whatever viscosity is chosen, maintaining the oil within the pump manufacturer's specified temperature range (typically 30-60 degrees Celsius) has a larger impact on service life than the specific ISO grade selected.
How does a servo-driven vane pump compare to an all-electric clamping unit?
An all-electric toggle-clamp system eliminates hydraulics entirely from the clamping circuit, using a servo motor and ball screw to generate clamping force. The advantages are zero hydraulic oil consumption for clamping, near-silent operation during clamp-up, and energy efficiency approaching 90% (versus 75-80% for a servo-hydraulic clamp). The disadvantages are higher initial cost (typically 25-40% more than an equivalent hydraulic clamp machine), mechanical complexity of the toggle linkage that requires precise lubrication and periodic rebuild, and a clamping force plateau limited by the ball screw's load capacity. For machines under 200 tons producing high-precision medical or electronic parts, all-electric clamping is often the right choice. For machines above 300 tons or those running abrasive materials where hydraulic robustness matters, a servo-driven vane pump system provides the best balance of precision, energy efficiency, and mechanical simplicity.
What is the most common failure mode for vane pumps in IMM clamping service?
Contamination-related cam ring wear is the most frequent failure mode, accounting for roughly 60% of vane pump failures in injection molding applications. The cam ring is the stationary outer ring against which the vanes slide — and because vane tip velocities can reach 8-10 m/s at full speed, even particles as small as 5-10 microns can cause erosive wear. The wear pattern is typically a polished groove at the major diameter of the cam ring where the vanes experience maximum radial force. Prevention is straightforward: maintain oil cleanliness at ISO 4406 18/16/13 through 10-micron absolute-rated return-line filtration, change filters on schedule (not on indicator alone — some plants push filter life too far), and perform oil analysis quarterly to catch contamination trends before they cause damage. The second most common failure — dry startup after extended shutdown — can be prevented by pre-filling the pump case with oil before restarting a machine that has been idle for more than 72 hours.