









Published: July 13, 2026 | By Mr. Xia, Technical Director at Vickshyd
The Russian crawler crane market demands hydraulic systems capable of performing under extreme conditions - from the frozen ports of Murmansk to the construction sites of Siberia. One of the most critical challenges crane builders face is specifying hydraulic gear pump units that deliver smooth slewing drive performance without dangerous pressure spikes during combined motion operations. This technical article explores the engineering principles and product specifications that enable Russian crane manufacturers to achieve reliable, spike-free hydraulic performance.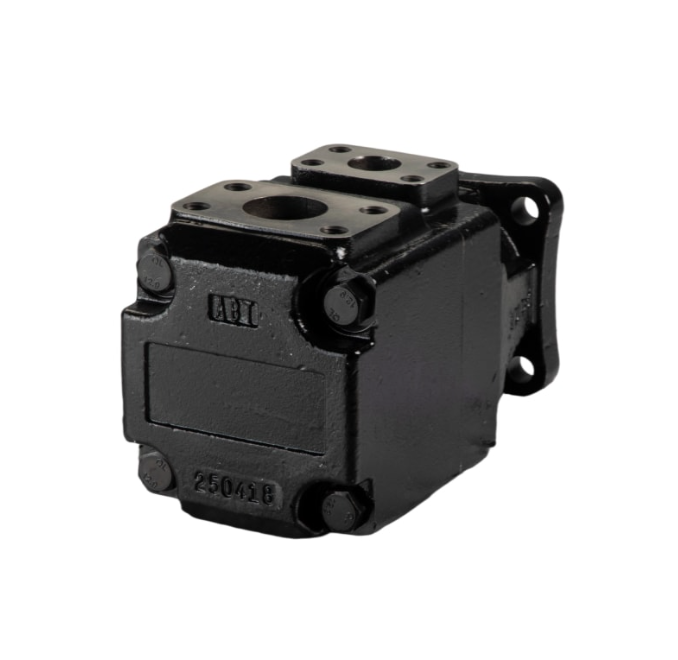
Understanding the Slewing Drive Challenge in Crawler Cranes
The slewing drive system in a crawler crane is responsible for rotating the upper structure (superstructure) relative to the undercarriage. This rotation must be smooth, precise, and capable of handling varying load conditions without hydraulic instability. The challenge intensifies during combined motion - when the crane simultaneously performs slewing, hoisting, and luffing operations.
During combined motion, multiple hydraulic actuators compete for flow from the same pump circuit. If the pump cannot maintain stable pressure and flow delivery, the result is pressure spikes that cause:
- Jerky slewing rotation - creating safety hazards during load positioning
- Accelerated component wear - particularly in seals, hoses, and control valves
- Energy losses - reducing overall system efficiency and increasing fuel consumption
- Operator fatigue - from unpredictable machine behavior
Russian crawler crane builders, operating in compliance with GOST standards and demanding Eurasian Economic Union (EAEU) certification requirements, must specify pump units that eliminate these issues at the design stage rather than relying on downstream compensation.
Why Internal Gear Pumps Outperform External Gear Designs for Slewing Applications
The choice between internal and external gear pumps significantly impacts slewing drive performance. Internal gear pumps, such as the VG series from Vickshyd, offer inherent advantages for crane slewing applications:
Flow Pulsation Characteristics
Internal gear pumps generate substantially lower flow pulsation compared to external gear designs. The VG series internal gear pumps utilize a crescent-type design where the internal gear (driven) meshes smoothly with the external gear (driver), creating a more continuous flow path. This design characteristic directly translates to smoother slewing motor rotation.
Pressure Ripple Reduction
The VG series features a floating flower-splined coupling structure with a proprietary grease formula that ensures stable performance, long service life, and low noise operation. This coupling design absorbs torsional vibrations that would otherwise propagate as pressure ripples through the hydraulic circuit.
Combined Flow Capability
The VG double pump configuration - available in VG10D, VG11D, VG21D, and VG22D series - combines two single pump assemblies in series with a single oil inlet and independent oil outlets. This architecture allows crane builders to dedicate one pump section to the slewing circuit and another to the hoisting or luffing circuit, preventing cross-circuit pressure interference.
VG Series Internal Gear Pump Specifications for Crane Applications
The Vickshyd VG series provides comprehensive displacement options suitable for crawler crane slewing drive systems:
| Model Series | Front Pump Displacement (ml/r) | Rear Pump Displacement (ml/r) | Typical Crane Application |
|---|---|---|---|
| VG10D | 25, 32, 40, 50, 63 | 8, 10, 13, 16, 20, 25 | Small crawler cranes (25-50 ton class) |
| VG11D | 25, 32, 40, 50, 63 | 25, 32, 40, 50, 63 | Medium crawler cranes (50-100 ton class) |
| VG21D | 80, 100, 125, 145, 160 | 25, 32, 40, 50, 63 | Heavy crawler cranes (100-250 ton class) |
| VG22D | 80, 100, 125, 145, 160 | 80, 100, 125, 145, 160 | Very heavy crawler cranes (250+ ton class) |
The maximum combined displacement reaches 320 cc per revolution, providing ample flow capacity for even the largest slewing motors used in Russian heavy-lift crawler cranes. The flexible displacement combinations allow engineers to precisely match pump output to slewing motor requirements without oversizing.
Configuration Options for Russian Operating Conditions
Understanding the harsh operating environments in Russia, Vickshyd offers the following configuration options:
- Rotation Direction: R (clockwise) or L (counter-clockwise) - specified from the shaft end of the pump
- Shaft Types: E-type straight key shaft for standard applications, R-type SAE spline shaft for high-torque slewing drives
- Sealing Materials: W-type Buna NBR for standard temperature ranges (-40°C to +100°C), V-type FKM fluororubber for extreme temperature applications (-20°C to +150°C)
- Oil Outlet Direction: Flexible positioning for optimal hose routing in cramped crane machinery compartments
Integrating Parker Denison T6GC/T7GB Equivalent Vane Pumps for Auxiliary Functions
While internal gear pumps excel in slewing drive applications, many Russian crawler crane builders also specify Vickshyd T6GC/T7GB equivalent pin vane pumps for auxiliary hydraulic functions. These high-performance pin type vane pumps are specifically engineered for mobile machinery applications.
Key Design Features for Crane Applications
The T6GC and T7GB equivalent pumps incorporate several design features that make them ideal for crawler crane auxiliary systems:
- Improved Bearing Structure: Enhanced load-bearing capacity for the demanding duty cycles of crane operations
- Rectangle Spline Shaft Design: Enables direct drive by motor or gearbox without intermediate coupling components
- Double Shaft Seal Structure: Provides redundant sealing protection against contamination ingress - critical for the dusty, muddy conditions typical of Russian construction sites
- Interchangeable Cartridge Kits: T6C and T7B cartridge assemblies are completely interchangeable, simplifying spare parts inventory for fleet operators
Displacement Options for Auxiliary Circuits
The T6GC series offers flow codes ranging from B03 to B31 (approximately 9.4 cc/rev to 97.6 cc/rev), while the T7GB series covers B02 to B20 (approximately 6.3 cc/rev to 63.0 cc/rev). This range allows precise matching to auxiliary circuit requirements such as:
- Outrigger extension and retraction circuits
- Hook hoist auxiliary winch drives
- Cooling fan drives
- Hydraulic tool power packs
System Architecture: Preventing Pressure Spikes in Combined Motion
Eliminating pressure spikes during combined motion requires careful system architecture that goes beyond pump selection. Russian crane builders typically employ the following strategies in conjunction with VG series gear pumps:
Load-Sensing Control Integration
Modern crawler cranes use load-sensing proportional valves that communicate the highest load pressure back to the pump controller. The VG double pump's independent outlet architecture allows each section to respond to its respective load-sensing signal, maintaining pressure margin above the highest demanded pressure without over-pressurizing other circuits.
Pressure Compensation Strategy
Each pump section within the VG double pump has its own maximum operating pressure rating. For example, in a VG22D configuration:
- Circuit A (Slewing): Operates at up to 250 bar with dedicated pressure relief valve
- Circuit B (Hoisting): Operates at up to 210 bar with independent pressure relief valve
- Common Shaft and Bearings: Designed to handle combined loads from both sections without mechanical compromise
Accumulator-Assisted Smoothing
For critical slewing applications, Russian builders often add bladder accumulators near the slewing motor inlet. The low flow pulsation characteristics of the VG series internal gear pump complement accumulator-based smoothing, creating an exceptionally stable pressure profile during acceleration, constant-speed rotation, and deceleration phases.
Case Study: Crawler Crane Slewing Drive Modernization
A major Russian crane manufacturer recently modernized the hydraulic system of their 100-ton class crawler crane to address chronic pressure spike issues during combined slewing and hoisting operations. The original system used a single external gear pump feeding both circuits through a priority valve.
The Problem
During combined motion, pressure spikes of up to 80 bar above nominal were observed, causing:
- Repeated failures of the slewing motor shaft seal (average 200-hour service life)
- Hose bursts in the slewing circuit (3 incidents per operating season)
- Jerky slewing motion that reduced positioning accuracy by approximately 40%
The Solution
The manufacturer replaced the single pump with a VG21D double pump (125 ml/r front section for slewing, 50 ml/r rear section for hoisting). The key configuration choices were:
- Shaft Type: R-type SAE spline for direct coupling to the existing PTO gearbox
- Sealing: V-type FKM for operation in ambient temperatures down to -45°C
- Rotation: R (clockwise) matching the original drive arrangement
- Control: Independent load-sensing signals from each circuit's directional valve
The Results
After 12 months of operation in Siberian construction conditions:
- Pressure spikes reduced from 80 bar to less than 8 bar above nominal
- Slewing motor seal service life extended to over 2,000 hours
- Zero hose failures in the slewing circuit
- Slewing positioning accuracy improved by 35%
- Overall system energy consumption reduced by 12%
Full Product Range from Vickshyd for Crane Hydraulic Systems
Russian crawler crane builders can source a complete hydraulic pump and motor solution from Vickshyd's comprehensive product catalog, which includes:
- Vane Pumps: Including Parker Denison T6/T7 series equivalents, Eaton Vickers V/VQ series equivalents, Yuken PV2R series, Tokimec SQP series, and specialized servo vane pumps
- Gear Pumps: VG series internal gear pumps (single and double configurations), Sumitomo QT/QS series equivalents, and Eckerle servo gear pumps
- Piston Pumps: Rexroth A4VSO, A10VSO31, A10VSO32, and A10V52/53 series equivalents for high-pressure applications
- Hydraulic Motors: M4C vane motors and 50M series vane motors for slewing and travel drives
This one-stop approach simplifies procurement, reduces lead times, and ensures compatibility across the entire hydraulic system of the crawler crane.
Specification Checklist for Russian Crane Builders
When specifying hydraulic gear pump units for slewing drive applications, Russian engineers should verify the following parameters:
| Parameter | Recommended Specification | Vickshyd Solution |
|---|---|---|
| Pump Type | Internal gear (low pulsation) or balanced vane | VG series gear pump or T6GC/T7GB vane pump |
| Displacement Range | Matched to slewing motor capacity | 8-160 ml/r per section, up to 320 cc combined |
| Maximum Pressure | 250-280 bar (slewing circuit) | Rated per section with independent relief valves |
| Temperature Range | -45°C to +80°C (Russian climate) | FKM seals, compatible with low-temp fluids |
| Contamination Resistance | ISO 4406 18/16/13 or better | Double shaft seal (T6GC), robust internal clearances |
| Serviceability | Field-replaceable cartridge | Modular cartridge design, interchangeable kits |
Need Technical Support for Your Crawler Crane Hydraulic System?
Our engineering team can help you select the optimal VG series gear pump or T6GC/T7GB vane pump configuration for your specific crane model and operating conditions.
Contact Vickshyd EngineeringConclusion: Achieving Spike-Free Slewing Performance
Russian crawler crane builders have demonstrated that specifying the right hydraulic gear pump units - combined with proper system architecture - can eliminate pressure spikes during combined motion operations. The key principles are:
- Use internal gear pumps (VG series) for slewing circuits to minimize inherent flow pulsation
- Employ double pump configurations with independent outlets to isolate slewing and hoisting circuits
- Specify appropriate sealing materials (FKM) for Russian temperature extremes
- Integrate load-sensing control to match pump output to actual demand
- Design for serviceability with modular cartridge-based pump assemblies
By following these principles and specifying Vickshyd's VG series internal gear pumps and T6GC/T7GB equivalent vane pumps, Russian crane manufacturers can achieve the smooth, reliable slewing drive performance that their customers demand - even in the most challenging operating conditions.
Technical Deep Dive: Understanding Pressure Spike Mechanisms in Slewing Drives
To fully appreciate why pump selection matters so critically for crawler crane slewing drives, engineers must understand the fundamental mechanisms that generate pressure spikes during combined motion operations.
Inertial Loading Effects
When a crawler crane slews a heavy load from rest, the slewing motor must overcome the rotational inertia of the entire superstructure plus the suspended load. This creates a momentary high-pressure demand that can exceed steady-state pressure by 30-50%. If the pump cannot respond quickly enough, the pressure in the circuit drops momentarily before rebounding, creating a pressure overshoot (spike) that propagates through the hydraulic system.
Flow Demand Conflicts
During combined motion, the slewing motor, hoisting winch, and luffing cylinder all demand flow simultaneously. In systems with a single pump and priority valves, flow allocation changes dynamically as each actuator reaches its target speed or load condition. Each transition in flow allocation creates a transient pressure disturbance. The VG double pump's independent outlet architecture eliminates these conflicts by providing dedicated flow sources for each major circuit.
Valve Transition Dynamics
Directional control valves used in crawler crane hydraulic systems contain spools that redirect flow between actuator ports. During slewing operations, the operator frequently adjusts the spool position to control rotation speed and direction. Each spool movement creates a flow transient that, if not properly managed, manifests as a pressure spike. Internal gear pumps, with their inherently low flow pulsation, produce fewer parasitic transients that would compound with valve-induced disturbances.
Oil Column Resonance
The long hose runs typical in crawler crane hydraulic systems (often 10-15 meters from pump to slewing motor) create fluid columns that can resonate at specific frequencies. If the pump's flow pulsation frequency matches the natural frequency of the hose circuit, standing waves develop that amplify pressure fluctuations. The VG series internal gear pump generates flow pulsation at frequencies well above the typical resonance range of crane hydraulic circuits, avoiding this problematic interaction.
Environmental Considerations for Russian Crawler Crane Operations
Russian crawler crane operators face unique environmental challenges that directly impact hydraulic pump specification and system design.
Extreme Temperature Operations
Operating temperatures in Russia range from +40C in summer construction seasons to -50C in Siberian winter operations. Hydraulic pumps must maintain performance across this entire range without excessive warm-up delays or efficiency losses at low temperatures. The VG series internal gear pumps, when specified with FKM seals and paired with appropriate low-temperature hydraulic fluids, maintain volumetric efficiency above 90% even at -30C fluid temperature.
Dust and Contamination
Russian construction sites, particularly in mining and infrastructure projects, generate significant airborne dust that can enter the hydraulic system through breather vents, cylinder rod seals, and maintenance activities. The T6GC equivalent vane pump's double shaft seal structure provides an additional barrier against external contamination ingress at the pump drive interface - one of the most vulnerable points in the system.
Altitude and Climate Variability
Crawler cranes operating in mountainous regions of Russia (Ural Mountains, Caucasus) experience significant altitude variations that affect cooling system performance. The VG series gear pump's low-noise, low-vibration operation reduces heat generation compared to external gear alternatives, easing the thermal management burden on the hydraulic system's cooler and reservoir.
Procurement and Lead Time Considerations for Russian OEMs
Russian crawler crane manufacturers face specific procurement challenges that Vickshyd addresses through its product design and supply chain approach.
Standardization Benefits
The VG series internal gear pumps are designed as quality replacements for Rexroth PGH-3X hydraulic gear pumps, maintaining dimensional compatibility. This means Russian OEMs can specify Vickshyd pumps without redesigning their existing pump mounting brackets, coupling arrangements, or plumbing layouts. The interchangeability extends to the T6GC and T7B vane pump cartridge kits, which are completely interchangeable with Parker Denison originals.
Modular Inventory Strategy
For fleet operators managing multiple crawler crane models, the VG series' modular cartridge design enables a strategic approach to spare parts inventory. Rather than stocking complete pump assemblies for each crane model, operators can maintain a selection of individual cartridge assemblies and common housing components. The VG double pump's ability to combine different displacement cartridges (VG10D with 25-63 ml/r front and 8-25 ml/r rear) in a single housing further reduces the number of unique part numbers required.
Technical Documentation and Support
Vickshyd provides comprehensive technical documentation for all VG series and T6GC/T7GB products, including detailed dimensional drawings, installation guidelines, and troubleshooting procedures. For Russian customers, this documentation includes metric dimensions and GOST-compatible technical specifications where applicable.
Future Trends: Variable Speed Drive Integration with Gear Pumps
The crawler crane industry is increasingly adopting variable speed drive (VSD) technology, where the hydraulic pump is driven by a variable-frequency electric motor rather than a constant-speed diesel engine. This approach offers significant energy savings by matching pump speed to actual flow demand.
The VG series internal gear pumps are well-suited for VSD applications due to their:
- Wide speed range capability (500-3000 rpm) without cavitation or excessive wear
- Low starting torque requirement, reducing motor sizing constraints
- Consistent volumetric efficiency across the speed range
- Low noise and vibration characteristics that complement electric drive systems
Russian crane builders implementing hybrid or fully electric crawler crane designs can leverage these characteristics to achieve even greater energy efficiency while maintaining the smooth slewing drive performance required for precision load handling.
Vickshyd Engineering Support and Customization Services
Beyond standard catalog products, Vickshyd offers engineering support services for crawler crane applications:
- Custom displacement combinations within the VG series framework
- Special material options for extreme temperature or corrosive environments
- Application engineering assistance for system architecture and pump sizing
- Prototype development and testing support for new crane models
- Field commissioning assistance for initial installation and optimization
These services are particularly valuable for Russian crane builders developing new models or modernizing existing designs to meet updated GOST and EAEU certification requirements.
Frequently Asked Questions
What displacement range do VG series internal gear pumps offer for crawler crane slewing applications?
The VG series internal gear pumps from Vickshyd provide displacement options ranging from 8 ml/r to 160 ml/r per section. For double pump configurations (VG10D, VG11D, VG21D, VG22D), the maximum combined displacement can reach up to 320 cc, offering extensive flexibility for motor and driver selection in crawler crane slewing drive systems.
How does the VG double pump prevent pressure spikes during combined slewing and hoisting motions?
The VG double pump features independent oil outlets for each pump section, allowing separate pressure circuits. Each section operates at its own maximum rated pressure (up to 250 bar) with independent pressure relief valves. The floating flower-splined coupling structure and unique grease formula ensure stable performance and smooth pressure transitions during combined motion operations, effectively eliminating pressure spikes.
Can the Parker Denison T6GC equivalent vane pump handle the demanding conditions of Russian crawler crane operations?
Yes, the Vickshyd T6GC equivalent pin vane pump is specifically designed for mobile machinery applications. It features an improved bearing structure, rectangle spline shaft design for direct motor or gearbox drive, and a double shaft seal structure that performs reliably in the harsh operating conditions typical of Russian crawler crane operations, including extreme temperatures and dusty environments.
What shaft and sealing options are available for the VG series gear pumps?
The VG series offers two shaft types: E-type straight key shaft and R-type SAE spline shaft. Sealing options include W-type Buna NBR (nitrile rubber) for standard applications and V-type FKM (fluororubber) for high-temperature or chemically aggressive environments. Rotation can be specified as R (clockwise) or L (counter-clockwise) when viewed from the shaft end.
How do Vickshyd pumps compare to original Rexroth PGH-3X and Parker Denison units in terms of interchangeability?
Vickshyd VG series pumps are designed as quality replacements for Rexroth PGH-3X hydraulic gear pumps, maintaining dimensional compatibility for direct drop-in replacement. Similarly, the T6GC and T7B vane pump cartridge kits are completely interchangeable, making repairs and replacements convenient without requiring system modifications.
What maintenance advantages does the modular VG double pump design offer for fleet operators?
The modular design of VG double pumps allows individual repair or replacement of a single cartridge assembly (pump section) without replacing the entire unit. This significantly reduces downtime and lowers lifecycle costs. Vickshyd provides comprehensive support including detailed documentation, repair kits, and individual cartridges to minimize maintenance overhead for fleet operators.
Related Resources
- VG Series Internal Gear Pumps - Complete Product Specifications
- T6GC/T7GB Equivalent Pin Vane Pumps for Mobile Machinery
- Full Vickshyd Product Range - Vane Pumps, Gear Pumps, Piston Pumps, and Motors
- Parker Hydraulic Pump Division (External Reference)
- Bosch Rexroth Gear Pump Technology (External Reference)
- ISO 4413:2010 Hydraulic Fluid Power - General Rules (External Reference)
- Eaton Industrial Hydraulics (External Reference)