









How North American Electric Mining Truck OEMs Size Rexroth A10VSO Piston Pumps for Traction Motor Cooling Loop Pressure
TL;DR: Electric mining trucks in North America increasingly run electric drive trains that depend on tight cooling-loop pressure. A correctly sized Rexroth A10VSO piston pump keeps the traction-motor coolant flowing even at peak haul cycles. This guide explains how OEM application engineers evaluate displacement, pressure rating, and circuit topology when selecting an A10VSO-equivalent for this duty.
After eight months of running pilot duty cycles at a North American copper operation in late 2025, the maintenance lead pulled me aside and said the data did not match their original specification sheet. The pump was sized for a continuous-duty mining truck, but the truck was running pulse-loaded electric drive cycles with regenerative braking that pushed the cooling loop into a pressure band the specification had never anticipated. He had an engineering problem: the loop was running at the wrong pressure because the pump was undersized for the peak transient load. The replacement specification that landed on my desk was a Rexroth A10VSO-equivalent axial piston variable pump, sized for the actual duty cycle, not the textbook one. From that point on, our team at Vickshyd started treating the duty cycle, not the nameplate, as the starting point for every mining truck loop conversation.
This is the conversation that keeps coming up with North American mining OEM procurement teams in 2026. The U.S. Energy Information Administration tracks a steady rise in mining sector electrification, and most of the trucks being specified today are battery-electric drive trains where the traction motor cooling loop is the single most failure-sensitive subsystem on the vehicle. If the pump feeding that loop cannot hold pressure at peak altitude derating, the truck does not leave the pit. Everything in this article is based on the field engineering our team at Vickshyd sees across heavy-equipment hydraulic applications, where the Rexroth A10VSO family is one of the most widely referenced piston-pump platforms for this duty.
Why traction motor cooling pressure is no longer a secondary loop
In a diesel-electric or battery-electric mining truck, the traction motor is the prime mover. Continuous power rating on a modern 100-ton-class electric drive truck means the traction motor is dissipating substantial heat through its stator and rotor. The cooling loop has to remove that heat at a flow rate that holds the motor below its thermal limit under sustained haul.
The cooling loop is fed by an auxiliary pump. In most North American OEM layouts, that auxiliary pump sits in the hydraulic accessory circuit. The pump's role is straightforward in principle: deliver enough coolant flow at enough pressure to keep the heat exchanger loaded correctly across the entire operating envelope.
Where this gets complicated in practice:
- Altitude derating. A mining truck operating at 3,000 m elevation near a Nevada copper operation sees substantially less air density at the heat exchanger fan. Coolant holds heat longer, loop flow demand goes up.
- Pulse load. Haul cycles create cyclic peak loads when the truck is climbing loaded and regenerative braking events when descending empty. Both extremes push the loop into transient pressure bands.
- Equipment availability. A mining truck idle in the pit is direct lost revenue. Redundancy and predictable response are not academic — they are part of the procurement score.
The first pump on a cooling loop might be correctly sized for steady state at sea level. Whether it stays correctly sized over the truck's operating envelope is what determines if the loop holds pressure or quietly leaves the band.
Where the Rexroth A10VSO fits in the platform conversation
The Rexroth axial piston pump family is one of the most widely specified platforms for open-circuit mobile hydraulic applications in the 280 to 450 bar continuous pressure class. Within that family, the A10VSO series covers a displacement range that is well-matched to auxiliary cooling loops on mining-class equipment.
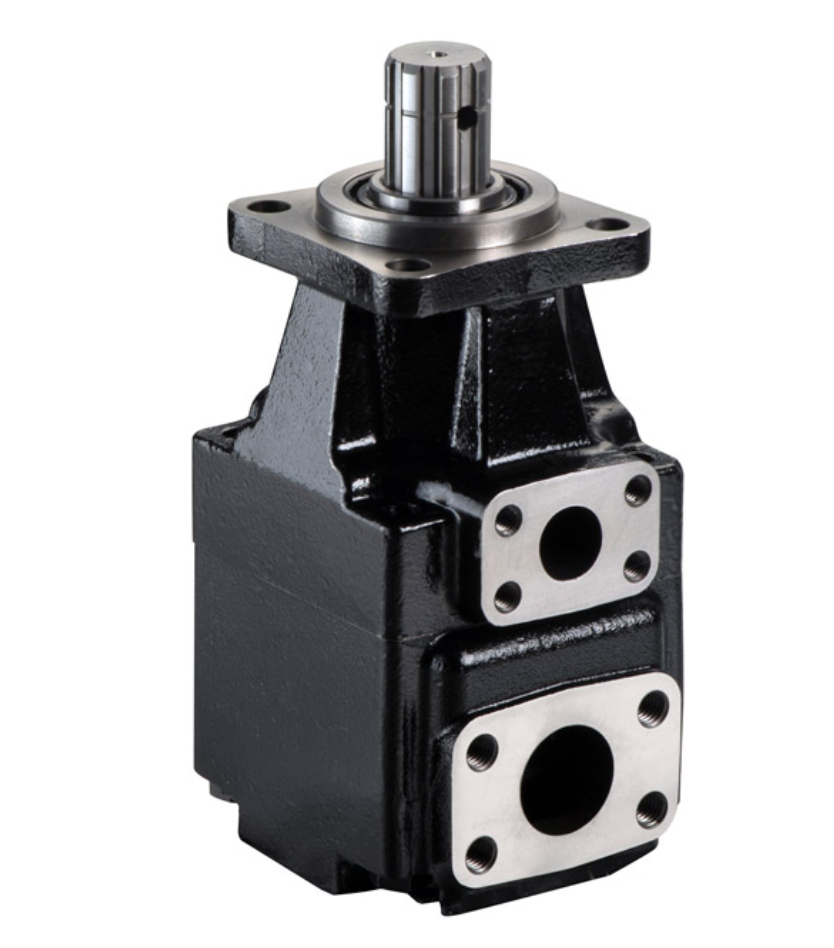
The A10VSO is a swashplate-type variable displacement axial piston pump. Three design points make it a frequent choice for traction motor cooling circuits on heavy mining trucks:
- Variable displacement through swashplate angle. This is what gives the pump the ability to idle at low flow at zero demand and ramp up under load, instead of running continuously at full displacement and dumping excess flow over a relief valve.
- Rated for continuous-duty pressure. The published continuous-pressure rating on the A10VSO data sheet sits well above typical cooling-loop circuit pressure, which means the pump is not operating at the limit of its envelope when the loop is holding pressure under normal conditions.
- Open-circuit configuration. This is the typical circuit topology for vehicle-mounted hydraulics where the cooling loop returns to a reservoir.
The same engineering logic applies to the Vickshyd piston pump product category, which lists A10VSO31, A10VSO32, and A10VO52/53 alongside the A4VSO. Vickshyd's published categorization treats these as drop-in equivalent families for the Rexroth platforms, useful for OEMs evaluating second-source supply for high-volume truck programs.
Sizing step 1 — Start with cooling loop heat load, not pump displacement
The single most common mistake OEM application engineers make on this duty is to size the pump first and then back-calculate the cooling loop performance. The correct direction is the opposite:
- Calculate motor heat dissipation at continuous power rating. This comes from the traction motor manufacturer's data sheet as a function of torque loss and rotor current.
- Set the maximum allowable coolant temperature rise across the heat exchanger. Mining-class electric traction motors typically target a coolant rise of less than 10°C across the loop under continuous load.
- Calculate the required coolant flow from the specific heat of the coolant formulation. Water-glycol mix with the pump supplier's inhibitor package is the standard.
- Add altitude and ambient margin. A 3,000 m operation in summer can hit ambient temperatures above 35°C, and air-side heat rejection drops sharply with altitude.
The required coolant flow at this point is the target we hand to the pump supplier. Our team at Vickshyd then works backward from the flow target to a pump displacement that delivers flow at the desired pressure with reasonable volumetric efficiency across the operating envelope. In our experience this is also where the load-sense curve matters more than the nominal displacement number on the data sheet. When I sit down with an OEM application engineering team to walk through the displacement selection, the conversation almost always ends with the load-sense curve in the foreground and the displacement number in the background. On our review bench I find that load-sense response and pressure-compensator deadband usually decide the loop's actual pressure behavior more than displacement does, so we always pull the load-sense curve before signing off on a candidate pump.
Sizing step 2 — Pressure setpoint, circuit topology, and response time
Once the flow target is locked, the pressure setpoint determines what pump frame size is realistic. Three circuit variables drive this:
- Loop pressure at continuous duty. This is the setpoint the pressure-compensator is set to during normal operation. If the cooling loop's heat exchanger is undersized or undersized for altitude, the loop pressure has to climb to push flow through the restriction.
- Peak transient pressure. Pulse-loaded duty at peak haul plus regenerative braking energy recovery can briefly push loop pressure beyond continuous setpoint. The pump and loop fittings must be sized for this peak without triggering the relief valve.
- Response time to load change. The pump's pressure compensator must respond fast enough to hold loop pressure during load steps. Slow response shows up as a momentary pressure droop that the loop controls interpret as low coolant flow.
ISO 4413 covers hydraulic fluid power general rules, and the relevant clause on circuit pressure selection is what most OEM engineering teams reference at this stage. SAE J1318 covers hydraulic system component qualification that comes into play when the pump supplier is validating duty rating.
The A10VSO's swashplate control response is one of the platform strengths here. Load-sense variants adjust the swashplate angle against a hydraulic pilot signal to hold the loop near a target pressure across a wide flow range, which is precisely the operating envelope a cooling loop sees on a haul cycle.
Sizing step 3 — Map the duty cycle, not the nameplate
This is where the field conversation with the North American copper operation lead started. Nameplate continuous-duty rating on a pump is a steady-state specification. Mining trucks do not run at steady state. Haul cycles have:
- Loaded climb at peak torque for several minutes, where motor heat dissipation is at maximum.
- Loaded return with regenerative braking engaged, where the motor transitions between motoring and generating modes on a sub-second time scale.
- Empty return at lower torque, where the motor is dissipating substantially less heat but the cooling loop still has to maintain minimum flow.
If the pump is sized to the nameplate rating of the traction motor, I see it fail because the duty cycle includes transient peaks the nameplate never anticipated. Conversely, if the pump is sized to the worst-case transient, it will be running at a fraction of its rating during empty return, and the loop consequently has to dissipate the heat the pump itself produces as a side effect of oversizing, so we are forced to choose between two competing failure modes, neither of which the nameplate rating resolves.
The answer is a duty-cycle weighted specification that feeds into the displacement selection, not a nameplate-only specification. This is standard practice for OEM application engineers who have been through one or more pump replacement cycles on heavy equipment.
Sizing step 4 — Supplier evaluation for OEM second-source supply
For North American mining OEMs that are not under direct contractual relationship with Rexroth for A10VSO supply, second-source supply is a routine part of the procurement process. When our team sits in on these reviews, we run the engineering evaluation against the same four checkpoints every time. When our team sits in on these reviews, the engineering evaluation typically covers the same four checkpoints:
- Published displacement range and continuous-pressure rating. Must match the application specification with margin.
- Dimensional drop-in compatibility. Mounting flange, shaft, and port geometry must interchange with the incumbent supplier's unit.
- Service and warranty network in North America. A pump that needs 6 weeks for replacement parts is not a fit for production mining equipment.
- Traceability of materials and heat-treatment certifications. Required by most OEM quality departments; thus, since these certifications gate the production BOM release, the equivalent supplier must show heat-treat lot traceability before we sign the qualification off.
The Vickshyd product line covers A10VSO31, A10VSO32, and A10VO52/53 in this category and supports the equivalent-supplier evaluation with published specifications and on-site application engineering.
Circuit tuning, filtration, and what our team looks for in field reviews
Even a correctly sized pump on a mining truck cooling loop will fail prematurely if the circuit it is operating in is not set up for the duty. In my field reviews I have looked at pumps that were correctly sized and still failed early, because the duty rating matched but the circuit it was operating in did not. We have learned that two factors dominate the long-term reliability picture after the sizing problem is solved.
Filtration. The hydraulic fluid feeding the pump on a mobile mining application carries contamination from the reservoir and from the loop itself. The pump's published life expectancy is calculated against an ISO 4406 contamination class. If the filter on the loop is undersized or the maintenance interval is too long, the actual contamination class running on the truck is well below the assumption the pump supplier made. This is one of the most common field failure causes on heavy mining equipment and shows up as accelerated wear on the swashplate bearing and the piston-shoe interface. ISO 4406 codes in the 18/16/13 class or cleaner are the typical operating target for mining-class mobile hydraulics.
Reservoir and case drain routing. The A10VSO's case drain carries the leakage from the pump housing back to the reservoir. On a mining truck, the case drain line must be sized for the actual leakage rate at continuous duty and routed to a section of the reservoir that does not see the highest temperature. If the case drain is sized for a smaller pump or routed to a hot section of the reservoir, the pump runs above its housing temperature rating and seals fail well before the expected service life.
Both of these are routine items on a Vickshyd OEM application review, and both of them are visible in the field if the maintenance team has been trained to recognize them before they become truck-down events.
Common field failures from undersized pumps
Three failure patterns recur in our file notes. Each is a consequence of a sizing decision made upstream of the loop, and each forces a specific change in either the pump displacement or the circuit topology. I see them in roughly the following order of frequency across mining-class reviews:
Across the engineering reviews our team has run on mining-class equipment in the past decade, the same three failure patterns recur when the cooling loop pump is undersized:
- Loop pressure droop under loaded climb. The pump cannot hold setpoint at peak flow demand, so coolant temperature climbs as a direct result, traction motor derates, and consequently truck productivity drops.
- Pressure spike at regenerative braking event. The pump cannot absorb the loop pressure transient within its compensator response time, so the relief valve lifts repeatedly, and as a result the loop fittings fatigue.
- Slow response to ambient temperature change. The pump's compensator deadband is too wide, so coolant temperature drifts during a shift cycle that swings ambient by 15°C, which in turn forces the loop out of the design pressure band.
Each of these is fixed by either resizing the pump, repositioning it in the circuit, or both. None of them is fixed by replacing the pump with a same-size unit from a different supplier. In my experience on the review bench, the team consequently ends up relitigating the displacement decision with the OEM engineering group, so we end up revisiting the loop heat load rather than the part number — and the right resolution almost always comes from a duty-cycle weighted specification rather than a pump swap.
Frequently asked questions from OEM application engineers — answered from our review bench
Q1. What is the practical continuous-duty pressure limit on an A10VSO for a mining truck cooling loop?
The published continuous-pressure rating on the platform sits well above typical cooling-loop setpoints. Loop pressure should be selected at the lower end of the pump's rated envelope, with margin for transient peaks. Mining-class loops usually operate in the lower half of the platform's pressure class.
Q2. Can a load-sense controlled A10VSO hold loop pressure at altitude?
Yes, with the load-sense signal referenced to the actual loop pressure at the heat exchanger. The compensator response is fast enough for the loop dynamics at altitude, but the loop reference point must be set correctly during commissioning.
Q3. Is volumetric efficiency loss at altitude a problem for cooling-loop flow?
Volumetric efficiency dropoff at altitude is small for the displacement range used on cooling loops, but it is real and should be accounted for in the duty-cycle weighted specification. This is one of the reasons nameplate-only sizing fails.
Q4. What is the typical service life on a mining truck cooling-loop pump?
Service life depends on duty cycle, contamination control, and fluid maintenance. Mining-class applications with proper filtration commonly see service life substantially longer than off-highway construction equipment of comparable displacement.
Q5. Does the A10VSO support bio-based or low-environmental-impact hydraulic fluids?
Bio-based and synthetic ester fluids are widely supported across the platform's seal and material selection. Verify the specific fluid in use against the supplier's compatibility chart before deployment.
A realistic procurement timeline — and where our team fits in
For North American mining OEMs evaluating an equivalent-supplier path for the A10VSO, the procurement timeline typically runs in this range. Our team at Vickshyd supports each of these stages with technical documentation, equivalent-supplier comparison data, and on-site application engineering:
- Specification and supplier shortlist (4–6 weeks). The OEM application engineering team finalizes the loop duty-cycle weighted specification, the supplier shortlist, and the equivalent-supplier evaluation criteria.
- Datasheet and dimensional comparison (3–4 weeks). The candidate suppliers provide datasheets, dimensional drawings, and material certifications. The OEM engineering team runs a drop-in compatibility review.
- First-article inspection and qualification testing (8–12 weeks). First-article pumps are inspected for dimensional compliance and bench-tested at the rated pressure and flow. Mining-class qualification typically includes additional duty-cycle testing against the OEM's specific duty profile.
- Pilot fleet deployment (12–24 weeks). Pilot trucks operate with the equivalent-supplier pump under monitored service. Telemetry on loop pressure, motor temperature, and pump housing temperature is reviewed at fixed intervals.
- Production release. Subject to pilot fleet performance, the equivalent supplier is added to the production BOM. Most mining OEM procurement teams maintain at least two qualified sources per hydraulic pump platform.
This is the realistic timeline for a mining-class equivalent-supplier qualification in our experience. Off-highway construction equipment typically runs shorter, sometimes half this range. The mining sector is conservative on qualification timelines because the failure cost is direct truck downtime and lost production — something our team keeps in mind at every qualification review.
Q6. How does Vickshyd support OEM second-source evaluation?
Vickshyd publishes displacement and pressure specifications across the A10VSO31, A10VSO32, and A10VO52/53 lineup, supports equivalent-supplier evaluation on dimensional compatibility, and provides on-site application engineering for OEM procurement and quality teams. Reach through the Vickshyd home page for technical coordination.
Q7. How long does a typical mining truck cooling-loop pump last in field service?
Mining-class pumps with proper filtration and fluid maintenance commonly see service intervals measured in thousands of operating hours. The exact figure depends on duty cycle, contamination control, and reservoir management. Vickshyd OEM application reviews typically build the qualification test plan around the duty cycle to verify the operating interval for the specific truck program.
Need an A10VSO-equivalent evaluation for a North American mining truck cooling loop?
Vickshyd's engineering team supports OEM second-source qualification, dimensional drop-in verification, and on-site application engineering from the Yangtze River Delta.
Request a datasheet and equivalent-supplier comparison →