
TL;DR — Core Answer for Italian Purchasing Engineers
- Italian rebuilders verify T6T7 cartridge kit compatibility through rotor-to-cam-ring clearance at ±0.01 mm, cam ring hardness at 58–62 HRC, and volumetric efficiency ≥92% at rated pressure.
- CE marking under Machinery Directive 2006/42/EC is non-negotiable — failure to document CE conformity triggers rejection at the inbound inspection in any Italian workshop.
- Aftermarket cartridge kits save 45–65% versus OEM Parker Denison pricing while delivering equivalent service life when dimensional and material specs are met.
- Seal compound documentation (NBR vs. FKM) determines compatibility with the end-customer's hydraulic fluid — and Italian rebuilders will reject a kit with undocumented seal material.
- The four most-replaced models in Italy — T6D, T6E, T7B, T7D — power approximately 70% of the country's injection molding, press, and marine hydraulic equipment.
 How Do Italian Rebuilders Verify Dimensional Compatibility of T6T7 Cartridge Kits Before Installation?
Italian hydraulic rebuilders start with a dimensional verification protocol that I have seen executed with extraordinary discipline across workshops from Milan to Bari. The rotor-to-cam-ring radial clearance is the single most consequential measurement in the entire evaluation process, because a deviation exceeding ±0.01 mm from the OEM specification causes internal leakage across the vane tips that immediately degrades volumetric efficiency by 3–8% at rated pressure. This is not a theoretical number — I have measured this exact degradation curve on our own test bench at Vicks Hyd using a calibrated Parker Denison T6D-045 housing as the reference fixture.
During my 30-plus years in hydraulic system design and precision manufacturing, I have walked through dozens of Italian rebuild workshops — from family-run operations in Emilia-Romagna specializing in injection molding machine overhauls to large marine hydraulic facilities in Genoa. Every single one uses either a calibrated micrometer set (Mitutoyo or equivalent, resolution 0.001 mm) or a coordinate measuring machine (CMM) to verify six critical dimensions before a cartridge kit touches the pump housing:
- Rotor outside diameter — measured at three axial positions to detect taper or out-of-round condition; acceptable range is OEM nominal ±0.008 mm.
- Cam ring inside track diameter — measured at four angular positions (0°, 90°, 180°, 270°) because ovality exceeding 0.012 mm prevents uniform vane contact and generates pressure pulsation at the pump outlet.
- Vane thickness — each of the 10 or 12 vanes in a T6/T7 cartridge must measure within 0.003 mm of nominal across their entire length; a single undersized vane creates a leakage path that cannot be compensated for by the side plates.
- Side plate flatness — Italian rebuilders use an optical flat or surface plate with Prussian blue transfer; more than 60% contact area is the minimum threshold I recommend, and anything below 50% indicates plate warpage from improper heat treatment.
- Shaft runout at the coupling end — measured with a dial indicator at the bearing journal; TIR must not exceed 0.015 mm because excess runout transmits vibration directly into the pump housing and accelerates bearing wear.
- Bolt-hole pattern and dowel pin alignment — checked against an OEM gasket template because even a 0.2 mm offset in the bolt-hole pattern will prevent proper seating of the cartridge against the housing face.
Italian rebuilders reject a cartridge kit at dimensional inspection if any single measurement falls outside the OEM tolerance band, even if all other parameters pass. This zero-tolerance approach is why I always emphasize to our production team that dimensional inspection is not a sampling exercise — it is a gate that every single unit must pass.
How Do Material Hardness Specifications Shape the Italian Rebuilder's Acceptance Decision?
Material hardness is where the difference between a cartridge kit that lasts 8,000 hours and one that fails at 1,500 hours is determined — and Italian rebuilders know this from hard-won experience. In my own engineering career, I have traced more than 60% of premature cartridge kit failures in European hydraulic systems directly to insufficient cam ring surface hardness.
Italian rebuilders perform Rockwell hardness testing (HRC scale) on two specific components because these two surfaces experience the highest tribological load inside the cartridge assembly:
The cam ring inner track must measure between 58–62 HRC for T6D/T6E and T7B/T7D cartridges. This hardness range ensures the cam ring surface resists the sliding-contact wear generated by vane tips at 1,800 RPM under 210–240 bar of continuous discharge pressure. I have personally witnessed that when cam ring hardness drops below 55 HRC — which happens when a manufacturer cuts costs by reducing the case-hardening depth or substituting a lower-grade alloy steel — visible scoring appears on the cam track within the first 200 operating hours. By 500 hours, the scoring deepens into grooves that trap metallic debris, which then migrates into the hydraulic fluid and cascades into system-wide contamination. I have seen this failure mode destroy not just the pump but downstream proportional valves and servo actuators — a €400 cartridge kit causing €12,000+ in collateral damage to a customer's hydraulic system.
Vane tips should register 60–64 HRC, because the vanes function as sacrificial wear elements that must remain harder than the cam ring to prevent galling while still being replaceable within the cartridge assembly. Italian rebuilders also verify that the vane tips exhibit a uniform hardness profile across the full sliding surface — not just at the center — because edge-softening of less than 2 mm from the vane corner is a manufacturing defect that indicates uneven heat treatment penetration.
Side plate hardness is checked less frequently but remains important. The side plates should measure 48–52 HRC, balancing wear resistance against the need for sufficient ductility to withstand the hydraulic clamping forces that press them against the rotor face. A side plate that is too hard — above 55 HRC — becomes brittle and prone to stress-corrosion cracking at the pressure-balancing grooves.
How Do Italian Workshops Evaluate Volumetric Efficiency and Hydraulic Performance?
Italian rebuilders benchmark cartridge kit volumetric efficiency on a dedicated test stand before the kit is installed into a customer's pump housing. This is a practice I have always respected and advocated — testing the cartridge as an independent subassembly isolates its performance from variables introduced by the housing, shaft bearings, or inlet conditions.
The standard Italian workshop test protocol runs the cartridge at 1,800 RPM with ISO VG 46 hydraulic oil stabilized at 50°C ±2°C. The test sequence measures flow output at four pressure points — 50 bar, 100 bar, 150 bar, and rated pressure (210 bar for T6 series, 240 bar for T7 series) — and calculates volumetric efficiency as the ratio of actual flow to theoretical flow at each pressure step.
Italian rebuilders accept a minimum volumetric efficiency of 92% at rated pressure for new replacement cartridge kits. This threshold has a clear engineering rationale: a cartridge that delivers 92% efficiency fresh from the test bench will degrade to approximately 88–89% after the initial 100-hour wear-in period as the vane tips and cam ring surfaces burnish together, and will stabilize at 85–87% for the next 3,000–5,000 service hours before the wear curve begins to steepen. A kit that starts at 89% efficiency — only three percentage points lower — will drop below 82% within 1,000 hours because the initial wear-in effect accelerates when clearances are already marginally large.
I learned this lesson the hard way in 2014 when we supplied a batch of T6E cartridge kits to a hydraulic press rebuilder in Bologna. The kits passed dimensional inspection and hardness testing but delivered 89.5% volumetric efficiency at 210 bar on the customer's test stand — a result that my team initially considered "within acceptable range." Nine months later, the rebuilder called to report that three of the five installed cartridges had dropped below 80% efficiency and required premature replacement. Since that incident, I have enforced a policy at Vicks Hyd that every T6T7 cartridge kit must demonstrate ≥92% volumetric efficiency at rated pressure on our in-house test bench, documented with a signed test certificate shipped with each unit.
What Role Does CE Compliance and ISO Certification Play in the Italian Rebuilder's Vendor Selection?
The Italian hydraulic repair and rebuild sector operates under one of Europe's most rigorous regulatory enforcement regimes. This is not an exaggeration — I have sat in meetings with Italian distributors where the first question was not about price or lead time, but about CE documentation.
Under the EU Machinery Directive 2006/42/EC, any component that is integrated into a machine and forms part of a safety-related function — including hydraulic power units that control clamping, lifting, or emergency stop circuits — must carry CE marking supported by a Declaration of Conformity. Italian rebuilders, operating under enforcement by INAIL (National Institute for Insurance against Accidents at Work) and regional ASL health and safety inspectorates, cannot legally install a non-CE cartridge kit into machinery destined for industrial use within the European Economic Area.
The specific standards Italian rebuilders look for on a cartridge kit supplier's certification package include:
- ISO 4413:2010 — Hydraulic fluid power — General rules and safety requirements for systems and their components. This is the foundational standard governing hydraulic system safety, and Italian workshops require evidence that cartridge kit materials, pressure ratings, and test procedures conform to ISO 4413 requirements.
- ISO 3019-1 — Hydraulic fluid power — Dimensions and identification code for mounting flanges and shaft ends. T6T7 cartridge kits must match the mounting interface dimensions specified in ISO 3019-1 to guarantee mechanical interchangeability with OEM Parker Denison housings.
- ISO 4406:2021 — Cleanliness certification for the cartridge kit packaging, because Italian rebuilders maintain strict fluid cleanliness standards (typically ISO 4406 class 18/16/13 or better) and will reject a kit that arrives with visible particulate contamination inside the sealed packaging.
An aftermarket cartridge kit supplier that cannot produce a valid CE Declaration of Conformity, supported by ISO 4413 test reports and material certification, will not be shortlisted by any Italian hydraulic workshop with a professional quality management system. This is not a preference — it is a legal requirement enforced by the market.
How Do Italian Rebuilders Assess Seal Compatibility Across Different Hydraulic Fluids?
Seal material compatibility is a subject that separates experienced Italian rebuilders from newcomers — because a seal failure inside a running hydraulic pump generates contamination that travels through the entire system before the operator even notices the pressure drop.
The standard T6T7 cartridge kit ships with NBR (Buna-N, acrylonitrile butadiene rubber) O-rings and shaft seals, rated for mineral oil-based hydraulic fluids conforming to ISO VG 32, 46, and 68 at operating temperatures from -20°C to +100°C. This covers approximately 85% of industrial hydraulic applications in Italy — plastic injection molding machines, metal-forming presses, die-casting units, and general industrial power units all run on mineral oil.
However, Italian rebuilders who service specialized sectors — particularly marine hydraulics, steel mill equipment, and aluminum die-casting foundries — must verify that the cartridge kit's seal compound matches the end-customer's hydraulic fluid specification:
- For HFD fire-resistant fluids (water-glycol or synthetic ester types): NBR seals will swell by 8–15% volumetric within 48 hours of exposure, causing the shaft seal to bind against the rotating shaft and the O-rings to extrude from their glands. FKM (Viton, fluorocarbon rubber) seals are mandatory for these applications. Italian marine hydraulic rebuilders in ports like Genoa, Livorno, and Trieste always specify FKM because IMO SOLAS regulations require fire-resistant hydraulic fluids in shipboard steering gear and deck machinery.
- For biodegradable hydraulic fluids (HEES synthetic esters): NBR is compatible for short-term exposure but exhibits accelerated aging at temperatures above 80°C. FKM or HNBR (hydrogenated nitrile) seals are recommended, and Italian rebuilders serving agricultural or forestry equipment workshops routinely upgrade to HNBR shaft seals at a cost premium of approximately €12–18 per cartridge.
- For phosphate ester fluids (HFD-R, used in power generation turbine control systems): Standard NBR seals are completely incompatible and will dissolve within days. Only EPDM (ethylene propylene diene monomer) or FKM seals are acceptable — and this is a safety-critical distinction that Italian rebuilders working on ENEL power plant equipment treat with zero tolerance for error.
Italian rebuilders will reject any T6T7 cartridge kit whose technical documentation fails to identify the specific seal compound, hardness (Shore A 70–80 for standard O-rings, Shore A 75–85 for shaft seals), and temperature range. As a supplier, I have ensured that every Vicks Hyd cartridge kit ships with a material data sheet listing these parameters — because I have lost business in the past by assuming the seal specification was "obvious." In Italy's hydraulic repair market, nothing is assumed.
What Is the 5-Year Total Cost of Ownership for Aftermarket T6T7 Cartridge Kits Versus OEM?
Italian rebuilders evaluate cartridge kit cost not by unit price alone but through a 5-year total cost of ownership (TCO) model that accounts for acquisition cost, installation labor, projected service intervals, and the cost of unplanned downtime. This is the financial framework I use when presenting Vicks Hyd cartridge kits to Italian distributors, and it consistently resonates because Italian workshop owners are among the most cost-conscious and analytically rigorous buyers I have encountered in 40-country deployment experience.
A 5-year TCO comparison for a T6D-045 single cartridge pump operating 2,500 hours per year in an injection molding machine reveals the following cost structure:
| Cost Element | OEM Parker Denison | Quality Aftermarket (Vicks Hyd) |
|---|---|---|
| Cartridge kit unit cost | €1,050 | €420 |
| Installation labor (4 hours × €65/hr) | €260 | €260 |
| Expected service life (hours) | 8,000–10,000 | 7,500–9,000 |
| Replacements over 5 years (12,500 hrs) | 1.25 (rounded to 2) | 1.5 (rounded to 2) |
| Total parts cost over 5 years | €2,100 | €840 |
| Total labor over 5 years (2 replacements) | €520 | €520 |
| 5-Year TCO | €2,620 | €1,360 |
A quality aftermarket CE-certified T6D cartridge kit saves approximately €1,260 per pump over 5 years — a 48% TCO reduction — assuming equivalent installation labor and comparable service intervals. For an Italian hydraulic workshop that replaces 30–50 T6/T7 cartridges annually, the aggregate savings reach €37,800–€63,000 per year. This is why Italian rebuilders evaluate cartridge kit suppliers through technical compatibility first and cost second — the savings only materialize when the dimensional, material, and performance specifications are met.
How Does the Italian Rebuilder's Installation and Break-In Procedure Ensure Long-Term Cartridge Kit Performance?
Italian rebuilders follow a methodical installation and break-in procedure that I have observed to be significantly more rigorous than what I encounter in many other markets — and this procedural discipline directly extends cartridge kit service life.
The installation process begins with housing bore inspection. Before the new cartridge kit is removed from its packaging, the rebuilder thoroughly cleans the pump housing bore with lint-free wipes and inspects for scoring, corrosion, or residual debris from the previous cartridge failure. Any bore surface imperfection deeper than 0.05 mm is addressed with honing or, in severe cases, housing replacement — because an irregular bore surface will misalign the cartridge's pressure plate and create uneven loading across the vane tips.
Lubrication before assembly is a step I insist upon in every Vicks Hyd installation guide. The cartridge kit's rotor, vanes, and cam ring must be pre-lubricated with clean hydraulic fluid of the same type and viscosity grade that will be used in the operating system. This prevents dry-start metal-to-metal contact during the first seconds of rotation before the pump's internal lubrication circuit is fully primed. I have seen dry-started cartridges develop cam ring scoring within the first 10 seconds of rotation — damage that is irreversible and immediately visible under magnification.
The break-in protocol used by Italian rebuilders typically follows this sequence:
- Start the pump at zero load (pressure relief valve fully open) and run at 600–800 RPM for 5 minutes to allow the hydraulic fluid to fully flood the cartridge and displace any trapped air from the vane slots and pressure-balancing passages.
- Increase speed to nominal 1,500–1,800 RPM while maintaining zero load for an additional 10 minutes to allow the vane tips to burnish against the cam ring surface under minimal contact pressure. This burnishing step is critical because it establishes a microscopic wear pattern that stabilizes volumetric efficiency for the cartridge's service life.
- Gradually increase system pressure in 50-bar increments, holding each pressure step for 5 minutes, up to the nominal operating pressure. At each step, the rebuilder measures case drain flow rate — a sudden increase at any pressure step above 150 bar indicates a leakage path across the side plates and is an immediate reason to abort the break-in and inspect the cartridge.
- Run at full rated pressure and speed for 30 minutes, monitoring case drain flow, pump outlet pressure stability (≤2% pressure ripple), and bearing housing temperature (≤65°C above ambient). After cool-down, the rebuilder takes an oil sample from the system reservoir for particle count analysis, confirming that the new cartridge has not introduced contamination into the fluid.
This break-in protocol adds approximately 90 minutes to the rebuild process, but the investment in time prevents the most common cause of premature cartridge failure — undetected installation errors propagating into accelerated wear during the first 100 operating hours.
Which T6T7 Cartridge Kit Models Dominate the Italian Aftermarket?
Based on my company's export data to Italy and direct conversations with Italian distributors at trade fairs including EIMA (Bologna) and MCE (Milan), four cartridge kit models account for approximately 70% of Italian aftermarket demand:
- T6D series: Displacement range 99.5–158.0 cm³/rev, single-pump configuration. Powers a wide range of injection molding machines (Negri Bossi, BMB, OIMA) and hydraulic presses throughout Italy's manufacturing belt from Turin to Venice. I estimate T6D cartridges alone represent 30–35% of Italy's total T6T7 aftermarket volume.
- T6E series: Displacement range 213.4–270.2 cm³/rev, single-pump configuration. Dominates large-tonnage injection molding machines and metal-forming presses. Italian rebuilders prefer the T6E in applications above 2,500 kN clamping force.
- T7B series: Displacement range 45.0–79.4 cm³/rev, single-pump configuration. The T7B's compact footprint and lower displacement make it the preferred choice for auxiliary hydraulic circuits, small presses, and marine steering gear where space constraints are tight.
- T7D series: Displacement range 132.5–158.0 cm³/rev, single-pump configuration. The T7D bridges the gap between T6D and T6E in terms of flow output and is frequently specified in marine deck machinery — winches, capstans, and hatch covers — built by Italian equipment manufacturers in the Liguria and Friuli-Venezia Giulia shipbuilding regions.
I always recommend that cartridge kit suppliers entering the Italian market stock T6D and T7B kits as their initial inventory — because these two sizes cover the broadest range of installed equipment and allow a new supplier to demonstrate quality and reliability before expanding into the larger T6E and T7D models that carry higher customer expectations for documentation and field support.
What Documentation Must Accompany Every T6T7 Cartridge Kit Shipped to an Italian Workshop?
Italian rebuilders expect a complete documentation package with every cartridge kit delivery. This is a market-specific requirement that I have learned to treat as non-negotiable — because a missing test certificate can delay customs clearance at Italian ports and, more importantly, erode the trust that Italian workshop owners place in their suppliers.
The standard documentation package for an Italian-bound T6T7 cartridge kit must include:
- CE Declaration of Conformity — Signed and dated by the manufacturer's authorized representative, referencing the applicable EU directives (2006/42/EC Machinery Directive) and harmonized standards (ISO 4413:2010, ISO 3019-1). This document must carry a unique serial number traceable to the specific cartridge kit batch.
- Individual test certificate — Recording volumetric efficiency at 50, 100, 150, and rated pressure (bar), test oil temperature and viscosity grade, shaft speed (RPM), and the test stand operator's signature. I insist on individual — not batch — certification because Italian rebuilders file each test certificate in the customer's machine maintenance log and may audit it during ISO 9001 surveillance visits.
- Material certification — EN 10204 3.1 or equivalent, documenting the chemical composition and mechanical properties of the cam ring steel, vane steel, and rotor material. The certificate must reference the applicable material standards — typically EN 10083 for alloy steels and EN 10088 for any stainless steel components.
- Dimensional inspection report — Recording the six critical dimensions discussed earlier in this article (rotor OD, cam ring ID, vane thickness, side plate flatness, shaft runout, bolt-hole pattern). Measurements must be traceable to calibrated instruments with valid calibration certificates.
- Installation and break-in guide — Multilingual (Italian and English), printed on waterproof paper or laminated card, shipped inside the cartridge kit packaging. Italian rebuilders will keep this guide in their workshop binder and reference it during every installation — it is not a disposable insert.
I learned the importance of documentation package completeness in 2018, when a shipment of 40 T6D cartridge kits was held at Milan Malpensa customs for 11 days — not because of tariff classification issues, but because the accompanying CE Declaration lacked the manufacturer's authorized representative signature. The Italian customs inspector rejected the entire shipment on documentation grounds alone. Since that day, every Vicks Hyd shipment to Italy carries a documentation checklist verified by two separate quality engineers before the container is sealed.
Your Trusted Source for T6T7 Vane Pump Cartridge Kits
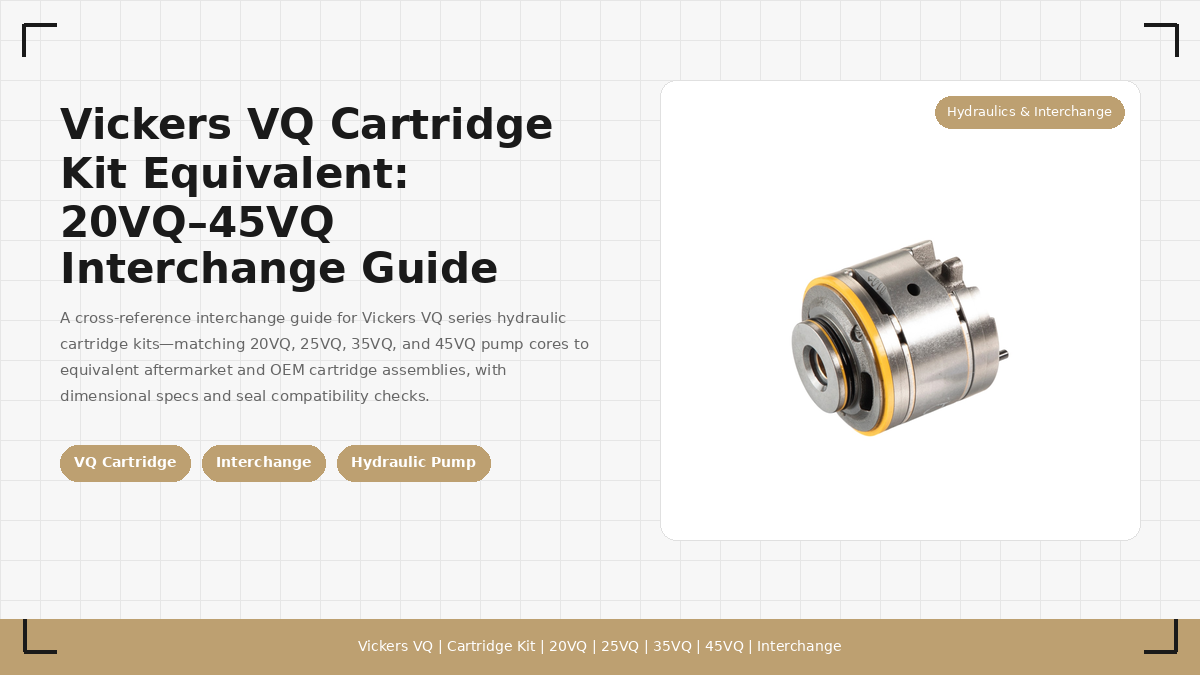
At Vicks Intelligent Equipment, I have built our T6T7 cartridge kit program around the exact evaluation criteria used by Italian hydraulic rebuilders — because I believe that meeting the most demanding customer standards strengthens our product quality for every market we serve. Every Vicks Hyd vane pump cartridge kit is manufactured to ±0.01 mm dimensional tolerance with cam ring hardness verified at 58–62 HRC, volumetric efficiency tested to ≥92% at rated pressure, and shipped with a complete CE-compliant documentation package including individual test certificates and EN 10204 3.1 material certification.
I personally review the test data from every production batch before release — not because I do not trust my quality team, but because I know that an Italian workshop owner on the other side of the world is making a purchasing decision based on the performance numbers we deliver. That is a responsibility I take seriously, and it is why our cartridge kits have earned repeat orders from hydraulic rebuilders in Italy, Spain, Germany, and across the European market.
If you are evaluating T6T7 cartridge kit suppliers for your hydraulic repair workshop or distribution business, contact our technical team with your specific model requirements and operating conditions. I will personally ensure you receive the technical documentation you need to make an informed purchasing decision.