
Eaton Vickers VQ Cartridge Vane Pump Sourcing for Ethiopian Cement Plant EPCs: How Procurement Teams Verify 24-Hour Cooler Kiln Duty and Altitude Derating at 2,400 Meters
Ethiopian cement plant EPCs operating at 1,800-2,800 meters elevation face two compounding thermal-management constraints that sea-level pump specifications don't address: 24-hour continuous-duty thermal load on the cooler kiln circuit, and altitude-induced reduction in convective cooling capacity. The Eaton Vickers VQ cartridge vane pump is widely specified for this duty class because of its cartridge serviceability under continuous dusty operation — but procurement teams need to verify four documentation checkpoints before signing the purchase order. This guide maps those checkpoints against the spec operating envelope and shows how to translate altitude derating into a revised thermal headroom figure.

Key Takeaways
- The Vickers VQ cartridge vane pump for Ethiopian cement plant EPC spec at Vicks Hydraulic covers the four procurement verification checkpoints for 24-hour cooler kiln duty at 2,400 meters altitude.
- Altitude derating at 2,400 meters reduces convective cooling capacity by 20-25%, requiring 15-20% derating of continuous-duty pump capacity or forced-air cooler specification to maintain equivalent thermal headroom.
- The Vickers VQ cartridge kit design enables in-field servicing without disturbing the pump housing or pipework — critical for cement plant continuous-duty maintenance windows where pipework disassembly is impractical.
- Procurement teams should verify four checkpoints: cartridge kit part number match to duty cycle, altitude-corrected thermal headroom, OEM continuous-duty test data at spec pressure, and OEM maintenance schedule for dusty-duty cartridge replacement.
- Single-stage VQ pumps are typically specified for cement plant cooler kiln duty at 100-175 bar continuous; double-stage versions extend to 350 bar continuous for high-pressure systems like cement mill roller presses.
- MOQ for Vickers VQ cartridge vane pumps from Chinese OEM manufacturers is 1-3 units for standard catalog ratings; EPC project quantities of 5-20 units commonly receive 10-15% per-piece reduction.
Table of Contents
This guide consolidates procurement verification economics for Eaton Vickers VQ cartridge vane pumps in Ethiopian cement plant EPC service, anchored to the Vicks Hydraulic product spec at Vickers Cartridge Vane Pump for Ethiopia Cement Plant EPC Spec.
24-Hour Cooler Kiln Duty Cycle
Cement plant cooler kiln hydraulic systems operate under one of the most demanding continuous-duty profiles in the cement industry. The cooler kiln conveyor hydraulics, grate cooler drive hydraulics, and cooler dust suppression hydraulics all run 24 hours per day, 7 days per week during production campaigns — typically 330+ days per year with brief maintenance shutdowns. The duty cycle is not the intermittent-duty profile typical of mobile equipment; it is a true continuous-duty profile that the pump must support without thermal shutdown.
Thermal Load Sources
The thermal load on the cooler kiln hydraulic circuit comes from three primary sources: (1) the pump's own internal leakage converting mechanical work to heat, (2) the throttling losses across the hydraulic control valves, and (3) the ambient heat ingress from the surrounding kiln environment. In a typical cooler kiln installation, the ambient temperature near the hydraulic power unit can reach 45-55°C during continuous operation, with radiant heat from the cooler structure adding 5-10°C to the local ambient at peak load.
The combined thermal load typically requires the hydraulic system to dissipate 25-40% of the pump's input power as heat. At continuous-duty ratings, this heat dissipation must be matched by the system's cooling capacity — which is where altitude derating becomes critical.
Dust and Contamination Exposure
Cooler kiln environments are dusty by nature. Clinker dust, cement raw mix dust, and ambient airborne particulates all find their way into the hydraulic reservoir through normal tank breathing. The Vickers VQ cartridge kit design addresses this by enabling scheduled cartridge replacement (typically every 4,000-6,000 operating hours under continuous dusty-duty conditions) without disturbing the pump housing, suction piping, or discharge piping. This is a critical advantage over fixed-cartridge vane pump designs that require full pump removal for vane replacement.
Duty Cycle Distinction
Continuous-duty specifications are fundamentally different from intermittent-duty specifications. A pump rated for intermittent duty (S2 or S3 per IEC 60034-1) at a given pressure and speed may not sustain the same ratings under continuous duty (S1) without thermal derating. Procurement teams specifying Vickers VQ pumps for cooler kiln service should explicitly require S1 continuous-duty rating data, not S2/S3 intermittent-duty data extrapolated to continuous operation.
Altitude Derating at 2,400 Meters
Ethiopian highland cement plants operate at elevations typically between 1,800 and 2,800 meters above sea level. At 2,400 meters — the typical mid-elevation operating point — the air density is approximately 77% of sea-level density. This 23% reduction in air density directly affects the convective heat transfer coefficient that governs hydraulic reservoir and oil cooler performance.
Heat Transfer Physics
Convective heat transfer from a hydraulic reservoir surface or oil cooler follows Newton's law of cooling: Q = h × A × ΔT, where Q is the heat dissipated, h is the convective heat transfer coefficient, A is the surface area, and ΔT is the temperature difference between the oil and the ambient air. The convective heat transfer coefficient h for natural convection depends on air density through the Nusselt number correlation; for forced convection (fan-cooled), h depends on air density through the Reynolds number.
At 2,400 meters, both the natural convection and forced convection coefficients decrease by approximately 23%, matching the air density reduction. The net effect is a 20-25% reduction in cooling capacity at the same ΔT, or equivalently a 20-25% increase in equilibrium oil temperature at the same heat dissipation load.
IEC 60559 and NEMA MG-1 Derating Standards
IEC 60559 and NEMA MG-1 provide standardized altitude correction factors for rotating equipment. For induction motors driving hydraulic pumps, the typical correction is 1% derating per 100 meters above 1,000 meters elevation. At 2,400 meters, the motor derating is approximately 14% relative to its sea-level rating. Hydraulic pump manufacturers apply similar derating curves to their continuous-duty performance data, with thermal derating typically steeper than motor derating due to the compounded effect of reduced cooling and increased oil viscosity at altitude.
| Elevation (m) | Air Density (% sea level) | Cooling Capacity (% sea level) | Recommended Derating |
|---|---|---|---|
| 0 (sea level) | 100% | 100% | None |
| 1,000 | 89% | 91% | 1-3% |
| 1,800 | 82% | 85% | 8-10% |
| 2,400 | 77% | 78% | 15-20% |
| 2,800 | 74% | 75% | 20-25% |
Practical Derating Application
Procurement teams applying the 15-20% derating at 2,400 meters have three practical options: (1) specify a larger pump displacement than the sea-level rating would suggest, accepting the upfront cost premium for continuous-duty headroom, (2) specify a forced-air oil cooler with altitude-corrected fan performance, accepting the auxiliary power consumption, or (3) specify a water-cooled heat exchanger (more effective at altitude than air-cooled), accepting the cooling water infrastructure requirement. Each option has cost-benefit tradeoffs that depend on the cement plant's overall utility infrastructure.
Cartridge Kit Design for In-Field Servicing
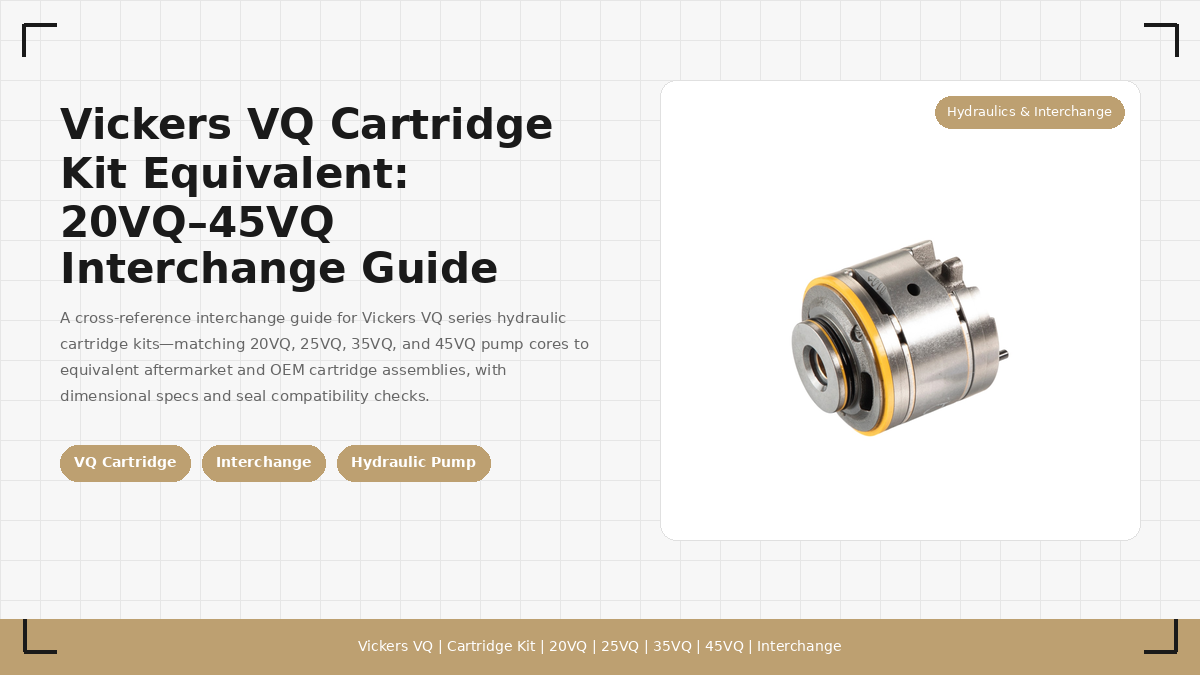
The Vickers VQ cartridge vane pump's defining feature is its removable cartridge kit — an integrated assembly containing the rotor, vanes, side plates, and internal porting that can be replaced as a unit without disturbing the pump housing, suction pipework, or discharge pipework. For cement plant continuous-duty service, this design provides four operational advantages over fixed-cartridge vane pump designs.
Advantage 1: Reduced Maintenance Window
Cartridge replacement typically takes 30-60 minutes per pump, compared to 4-8 hours for fixed-cartridge pump overhaul (which requires pump removal, pipe disconnection, and re-installation). For a cement plant operating 330+ days per year, each maintenance hour saved translates directly into production uptime. Across a fleet of 10-20 VQ pumps per cement plant line, the cumulative maintenance time savings justify the cartridge kit premium within the first 2-3 years of operation.
Advantage 2: No Pipework Disturbance
Fixed-cartridge vane pumps require suction and discharge pipe disconnection for vane replacement, which introduces contamination risk during reassembly. The cartridge kit design eliminates this risk by keeping the pump housing permanently installed in the pipework. The cartridge slides in and out of the housing without breaking any hydraulic connections.
Advantage 3: Predictable Service Intervals
Cartridge kit service intervals are predictable based on operating hours and duty cycle. For continuous-duty cooler kiln service at the spec pressure, the cartridge replacement interval is typically 4,000-6,000 hours (approximately 6-9 months of continuous operation). Procurement teams can pre-stock cartridge kits based on the cement plant's planned operating schedule, ensuring that replacement cartridges are on hand before scheduled maintenance windows.
Advantage 4: Field-Serviceable Without Specialized Tools
Cartridge replacement requires only standard hand tools (socket wrenches, torque wrench, clean workspace) — no specialized hydraulic press or alignment fixtures. Cement plant maintenance crews can perform cartridge replacement without calling in OEM service technicians, reducing the per-event maintenance cost by 60-70% compared to OEM-service cartridge replacement on fixed-cartridge designs.
Four Procurement Verification Checkpoints
Procurement teams sourcing Vickers VQ pumps for Ethiopian cement plant EPCs should verify four documentation checkpoints before signing the purchase order. Skipping these checkpoints risks post-installation thermal shutdowns, premature cartridge wear, or specification mismatches that surface only after commissioning.
Checkpoint 1: Cartridge Kit Part Number Match
Confirm that the cartridge kit part number specified in the purchase order matches the cooler kiln duty cycle requirements. The cartridge part number encodes the displacement rating, the vane material, and the side plate specification. For continuous-duty cooler kiln service, the cartridge should be specified with high-temperature vane material (typically carbon-graphite or reinforced phenolic) rather than standard glass-fiber-reinforced phenolic, which has a lower continuous-duty temperature ceiling.
Checkpoint 2: Altitude-Corrected Thermal Headroom
Verify the pump's altitude-corrected thermal headroom against the cement plant's specific elevation. The pump manufacturer's continuous-duty performance curves typically reference sea-level conditions; for elevated sites, the curves must be re-plotted with the altitude correction factor applied. Procurement teams should request altitude-corrected performance curves from the manufacturer for the specific elevation (e.g., 2,400 meters), not generic sea-level curves.
Checkpoint 3: Continuous-Duty Test Data
Audit the manufacturer's continuous-duty test data at the actual operating pressure and ambient temperature. The test report should include: (a) the test pressure, (b) the test ambient temperature, (c) the test speed (RPM), (d) the measured equilibrium oil temperature, (e) the measured volumetric efficiency over the test duration, (f) the test duration (typically 500+ hours for continuous-duty qualification). For Ethiopian cement plant applications, the test should be conducted at an ambient temperature of at least 45°C to reflect the actual operating environment.
Checkpoint 4: Maintenance Schedule for Dusty Duty
Request the OEM's recommended maintenance schedule for cartridge replacement under continuous dusty-duty conditions. The schedule should specify the cartridge replacement interval (operating hours), the recommended hydraulic fluid change interval, the recommended filter change interval, and the recommended reservoir breather specification for dusty environments. For cement plant cooler kiln service, the breather specification should be a desiccant-type or filtration-type breather rather than a standard unsealed breather.
Continuous-Duty Thermal Headroom Validation
Thermal headroom validation is the final step in procurement verification. The thermal headroom is the difference between the maximum permissible oil temperature (typically 80-90°C for standard hydraulic fluids, 95-100°C for high-temperature fluids) and the predicted equilibrium oil temperature at the spec operating condition.
Thermal Headroom Calculation
The thermal headroom is calculated using the pump's heat generation rate (proportional to the input power and the pump's inefficiency), the system's cooling capacity (proportional to the heat transfer surface area, the temperature difference, and the convective heat transfer coefficient), and the ambient temperature. At 2,400 meters, the convective heat transfer coefficient is reduced by approximately 23%, which directly reduces the cooling capacity and tightens the thermal headroom.
| Operating Condition | Sea Level Headroom | 2,400m Headroom | Recommended Action |
|---|---|---|---|
| 100 bar, 35°C ambient | 25-30°C | 20-24°C | Acceptable |
| 140 bar, 45°C ambient | 15-20°C | 10-14°C | Specify forced-air cooler |
| 175 bar, 50°C ambient | 8-12°C | 4-7°C | Specify water-cooled heat exchanger |
| 210 bar, 55°C ambient | 2-5°C | Negative | Re-spec or select higher thermal class |
Negative Headroom Mitigation
If the altitude-corrected thermal headroom calculation returns a negative value (meaning the equilibrium oil temperature would exceed the permissible maximum), the procurement specification must be revised. Options include: (1) selecting a pump with a larger displacement and operating at a lower percentage of its maximum rating, (2) specifying a higher thermal class fluid (synthetic ester rather than mineral oil), (3) specifying a water-cooled heat exchanger with adequate capacity at the spec elevation, or (4) selecting a different pump model with a higher continuous-duty thermal rating.
Single-Stage vs Double-Stage Selection
Single-stage Vickers VQ pumps deliver flow at the rated pressure in a single pumping chamber; double-stage (or two-stage) VQ pumps combine two pumping chambers to deliver higher pressure ratings at the cost of additional complexity. The selection between single and double stage depends on the cement plant circuit's pressure requirements.
Single-Stage Applications
Single-stage VQ pumps are typically specified for pressures up to 175 bar continuous / 210 bar peak. This covers most cement plant cooler kiln circuits, including cooler conveyor hydraulics (typically 100-140 bar), grate cooler drive hydraulics (typically 120-160 bar), and cooler dust suppression hydraulics (typically 80-120 bar). For these applications, single-stage VQ pumps offer the best balance of cost, efficiency, and serviceability.
Double-Stage Applications
Double-stage VQ pumps extend the continuous-duty pressure rating to 350 bar, with peak pressures to 420 bar. This covers high-pressure cement plant circuits like cement mill roller presses (typically 250-350 bar) and high-pressure material handling hydraulics. Double-stage VQ pumps cost 2-3 times more than equivalent single-stage units, so they are specified only when the pressure requirement exceeds the single-stage rating.
Selection Tradeoffs
The single-stage vs double-stage decision should be made based on the maximum continuous-duty pressure in the cement plant circuit, not the peak pressure. If the maximum continuous-duty pressure exceeds 175 bar, double-stage is required; otherwise, single-stage is the more cost-effective choice. Procurement teams should also consider the cartridge kit cost difference: single-stage cartridge kits are typically 40-50% cheaper than double-stage cartridge kits, so the total cost of ownership favors single-stage for cooler kiln duty.
MOQ, Lead Time, and EPC Project Logistics
MOQ and lead time considerations for Vickers VQ pumps in EPC project quantities differ from standard catalog purchases. Procurement teams managing multiple cement plant projects should plan their procurement strategy accordingly.
Standard Catalog MOQ
Standard catalog MOQ for Vickers VQ cartridge vane pumps is 1-3 units for in-stock displacement ratings. Lead times for in-stock units are typically 30-45 days from order confirmation, including factory testing and export documentation. For custom specifications (non-standard displacement, custom porting, special vane material), MOQ increases to 5-10 units and lead times extend to 60-90 days.
EPC Project Volume Discounts
EPC project quantities of 5-20 units per cement plant line commonly receive 10-15% per-piece reduction. Mixed-displacement orders across 2-3 displacement ratings can achieve 12-18% reduction by allowing the manufacturer to consolidate production scheduling. Bulk procurement for fleet operators managing multiple cement plants (20+ units across 2-3 plants) typically receives 15-25% per-piece reduction.
Spare Cartridge Kit Strategy
Procurement teams should plan spare cartridge kit inventory as part of the initial procurement. The recommended spare ratio is 1 cartridge kit per 2-3 pumps in service, ensuring that replacement cartridges are on hand when scheduled maintenance is due. Cartridge kits have a 5-year shelf life when stored in original packaging, making pre-stocking cost-effective for fleet operators.
Export Documentation for Ethiopian Delivery
Export documentation for Ethiopian cement plant delivery typically includes: commercial invoice, packing list, certificate of origin (China), hydraulic test certificate, material certificate (for pressure-bearing components), and Ethiopian customs documentation (including pre-shipment inspection certificate for capital goods). The pre-shipment inspection is typically conducted by an internationally recognized inspection agency (SGS, Bureau Veritas, or Intertek) at the manufacturer's facility before shipment.
Closing Note
Procurement teams sourcing Eaton Vickers VQ cartridge vane pumps for Ethiopian cement plant EPCs should apply a four-checkpoint verification framework: cartridge kit part number match to duty cycle, altitude-corrected thermal headroom validation against the cement plant's specific elevation, OEM continuous-duty test data at the spec operating pressure and ambient temperature, and OEM maintenance schedule for dusty-duty cartridge replacement. The Vicks Hydraulic product spec at Vickers Cartridge Vane Pump for Ethiopia Cement Plant EPC Spec supports this verification framework with documented altitude-corrected thermal headroom data, continuous-duty test reports, and EPC project MOQ flexibility. Procurement teams that apply all four checkpoints consistently avoid post-installation thermal shutdowns and premature cartridge wear, ensuring that the cement plant's cooler kiln hydraulic system operates at the spec production rate from day one of commissioning through the full design life of the EPC project.
References: This article references hydraulic pump altitude derating standards from IEC 60559 and NEMA MG-1, continuous-duty classification standards from IEC 60034-1, and product specifications linked to the Vicks Hydraulic Vickers VQ cartridge vane pump range.