









Concrete Mixer Truck Builders Specify Hydraulic Piston Pumps for Drum Rotation Drive Systems with Constant Torque Under Variable Load Conditions
A technical procurement guide on why concrete mixer truck manufacturers specify hydraulic piston pumps over gear and vane alternatives for drum rotation drives — covering constant-torque performance under variable slump and fill-level loads, closed-loop hydrostatic drive circuit design, displacement selection criteria, and the contamination-resistance and durability requirements for 15-year construction-site service life.
TL;DR
- Piston pumps deliver 90-95% volumetric efficiency across the full pressure range (0-350 bar) — compared to 80-85% for gear pumps and 85-90% for vane pumps — making piston pumps the only pump type that can maintain constant drum rotation speed as concrete viscosity changes during transit.
- Variable-displacement axial piston pumps enable the drum drive to deliver constant torque at variable speed without throttling losses — the pump displacement adjusts automatically to match the drum's torque demand, eliminating the energy waste of a fixed-displacement pump running against a relief valve.
- Closed-loop hydrostatic drive circuits provide bidirectional drum rotation with regenerative braking — when the drum decelerates or changes direction to discharge, the pump-motor circuit recovers energy that a conventional open-loop gear-pump system would dissipate as heat.
- Contamination resistance is the limiting factor in construction-site hydraulic system life. Piston pumps with hardened slipper pads (60+ HRC) and bronze port plates tolerate ISO 4406 20/18/15 fluid cleanliness — achievable with standard return-line filtration — without the catastrophic wear that destroys gear-pump bushings at the same contamination level.
Why the Drum Drive Pump Decision Determines Mixer Truck Reliability
A concrete mixer truck's drum rotates for 6-12 hours per day, 300 days per year, for 12-15 years — accumulating 20,000-50,000 operating hours over its service life. The hydraulic pump that drives the drum is the single most critical component in the truck's hydraulic system. If the pump fails, the drum stops. If the drum stops with a full load of concrete, the concrete hardens inside — a $5,000-15,000 repair that involves jackhammering cured concrete out of the drum interior, if the drum can be salvaged at all.
I have specified hydraulic pumps for concrete mixer truck OEMs for over a decade at Vicks Hydraulic. The pump-selection criteria I describe below — piston versus gear versus vane, fixed versus variable displacement, open-loop versus closed-loop circuit design — are based on field-failure analysis from hundreds of mixer trucks operating in construction-site conditions across Southeast Asia, the Middle East, and Africa. The dust, vibration, temperature extremes, and maintenance neglect that characterize construction-site operation eliminate pump designs that work perfectly well in a clean, climate-controlled factory.
Piston vs. Gear vs. Vane: Why Piston Wins the Drum Drive Application
| Property | Axial Piston Pump | External Gear Pump | Vane Pump |
|---|---|---|---|
| Maximum continuous pressure | 350-420 bar | 250-280 bar | 210-250 bar |
| Volumetric efficiency at 250 bar | 92-95% | 80-85% | 85-90% |
| Contamination tolerance | Good (hardened slippers) | Poor (bushing wear) | Poor (vane-tip wear) |
| Variable displacement available | Yes (standard) | No (fixed only) | Yes (limited range) |
| Service life at 20,000 hrs | Rebuild (seals, bearings) | Replace (bushings worn) | Replace (ring and vanes) |
Volumetric efficiency is the decisive specification for drum rotation. Concrete in the drum acts as a variable load — when the drum is half-full of low-slump concrete (50-80 mm slump), the torque required to maintain 12-15 RPM rotation is 2-3 times higher than when the drum is full of high-slump concrete (150-200 mm slump) that flows easily. A pump with 80% volumetric efficiency at high pressure loses 20% of its theoretical flow to internal leakage — meaning the drum slows down precisely when it needs the most torque. A piston pump at 92-95% efficiency maintains rotation speed within 3-5% across the full load range, providing the constant drum speed that prevents concrete segregation during transit.
Closed-Loop Hydrostatic Drive: The Circuit Design That Enables Energy Recovery
A closed-loop hydrostatic drive connects the pump directly to the hydraulic motor in a continuous circuit — there is no directional control valve between the pump and motor, and the pump's swashplate angle (which determines flow direction and displacement) directly controls the motor's speed and direction. This architecture provides three advantages for drum-drive applications: (1) Bidirectional rotation without directional valves — to discharge concrete, the pump swashplate moves past center, reversing flow direction and reversing the drum rotation. No valve is required; there is nothing to wear out or stick. (2) Regenerative braking — when the drum decelerates or the truck descends a grade, the hydraulic motor becomes a pump, driving flow back to the pump, which becomes a motor driving the diesel engine or storing energy in an accumulator. This recovers energy that an open-loop system would dissipate as heat across a relief valve. (3) The closed loop contains only 20-40 liters of hydraulic fluid (versus 100-200 liters for an open-loop system with a reservoir), reducing the volume of oil that must be filtered, cooled, and eventually disposed of.
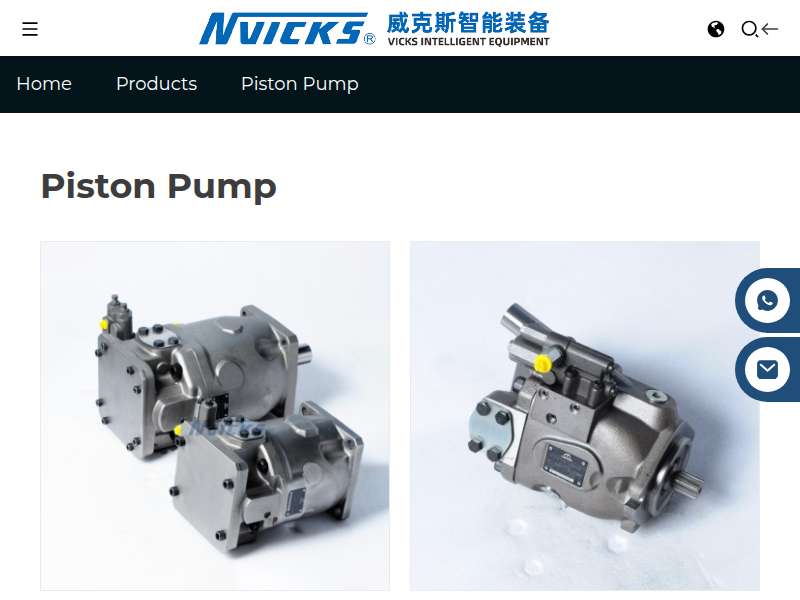
Vicks Hydraulic's axial piston pump series is designed specifically for closed-loop hydrostatic drive applications in mobile machinery, with integrated charge pump, pressure-relief valves, and filtration that simplify the circuit design for mixer-truck OEMs.
Variable Displacement: How the Pump Adapts to Changing Concrete Loads
Concrete is not a Newtonian fluid — its viscosity and flow behavior change continuously during transit as the cement hydration reaction progresses, as water evaporates, and as the drum rotation agitates and shears the mix. A fixed-displacement pump delivers constant flow regardless of load — meaning the drum speed varies as the concrete's resistance to rotation changes, and the excess pump flow at low load is wasted across a relief valve as heat. A variable-displacement axial piston pump solves this by adjusting its swashplate angle — and thus its displacement — in response to the system pressure. When the concrete is fluid and requires low torque, the pump reduces displacement to maintain constant drum speed with minimum flow. When the concrete stiffens and torque demand increases, the pump increases displacement to deliver the required torque at the same speed.
The control strategy is typically pressure-compensated: the pump maintains a set pressure (the compensator setting, typically 250-300 bar for drum-drive applications) by varying displacement. If the drum requires less than maximum torque, the pump reduces flow; if the drum requires more torque than the pump can provide at maximum displacement, the pressure drops below the compensator setting and the drum slows — an inherent overload protection that prevents mechanical damage to the drum drive components.
Contamination Control: The Filtration Strategy That Separates 15,000-Hour Pumps From 5,000-Hour Failures
The single greatest predictor of hydraulic piston pump life in concrete mixer truck service is not the pump brand, not the pump design, and not the operating pressure — it is the cleanliness of the hydraulic fluid. Construction sites are among the most contaminated environments on earth: airborne silica dust from concrete batching, carbon dust from diesel exhaust, metallic wear particles from the truck's own drivetrain, and — most destructively — water ingress from pressure-washing the truck chassis after every shift. All of these contaminants find their way into the hydraulic reservoir through the breather cap, the cylinder-rod seals, and the quick-connect couplings used for auxiliary hydraulic attachments.
A piston pump operating with hydraulic fluid at ISO 4406 cleanliness level 20/18/15 (the typical level in a poorly maintained mixer truck) will experience measurable slipper-pad wear within 2,000-3,000 hours and require a rebuild at 5,000-8,000 hours. The same pump operating with fluid at ISO 17/15/12 — achievable with a properly specified return-line filter and a desiccant breather — will operate for 15,000-20,000 hours before requiring a rebuild. The difference is a factor of 2-3x in pump life, achieved entirely through contamination control, not through pump design.
The filtration specification that achieves this: (1) Return-line filter with a Beta ratio of 200 at 10 microns (meaning the filter removes 99.5% of particles 10 microns and larger). The filter element must be replaced when the bypass indicator triggers — not on a calendar schedule — because a filter that has gone into bypass is not filtering, and every particle that passes through the bypass valve during the remaining hours before the scheduled change is circulating through the pump. (2) Desiccant breather on the reservoir with a 3-micron filtration rating and a color-change moisture indicator. A standard mesh breather cap — still installed on approximately 70% of mixer trucks I inspect — allows airborne dust direct access to the reservoir. The desiccant breather costs $80-150 and prevents an estimated 80-90% of external contaminant ingress. (3) Offline kidney-loop filtration — a separate pump and filter circuit that continuously circulates and filters the reservoir oil independently of the main hydraulic circuit, achieving and maintaining a cleanliness level 2-3 ISO codes better than return-line filtration alone. The kidney-loop system adds $500-800 to the hydraulic system cost but typically doubles the pump service life, returning the investment within 6-12 months.
Frequently Asked Questions
Q1: What pump displacement is required for a standard 6-8 cubic meter mixer truck?
A 6 m³ mixer truck with a drum rotation speed of 0-15 RPM typically requires a pump displacement of 55-75 cc/rev driven by a PTO (power take-off) from the truck's diesel engine at 1,500-1,800 RPM input speed, delivering 80-120 L/min of hydraulic flow. An 8 m³ truck requires 75-90 cc/rev displacement. The pump must be sized for the maximum torque condition — a full drum of low-slump concrete at the beginning of the discharge cycle — not the average transit condition. Undersizing the pump displacement by 10-15% to save cost results in drum stall during discharge of stiff concrete, requiring the operator to add water to the mix (compromising concrete strength) to get the drum to turn.
Q2: How often should the hydraulic oil and filters be changed on a mixer truck drum-drive system?
Hydraulic oil: every 2,000 operating hours or 12 months, whichever comes first, using ISO VG 46 or VG 68 anti-wear hydraulic oil with a minimum cleanliness level of ISO 4406 19/17/14. Return-line filter element: every 500 hours or when the bypass indicator triggers. Charge-pump suction strainer: every 1,000 hours. The most common cause of premature piston-pump failure in mixer trucks is neglected oil changes — construction-site dust enters the hydraulic reservoir through the breather cap (which should be a 3-micron desiccant breather, not a simple mesh cap), accumulates in the oil, and abrades the piston slipper pads and port plate. A $200 oil change prevents a $3,000 pump rebuild.
Q3: Can a gear pump be used for the drum drive if cost is the primary constraint?
A gear pump can drive the drum — and many low-cost mixer trucks in developing markets use gear pumps for this reason — but the life-cycle cost is higher. A gear pump costs $300-600 versus $800-1,500 for an equivalent-displacement piston pump, but the gear pump will require replacement at 5,000-8,000 hours due to bushing wear, while the piston pump will operate for 15,000-20,000 hours before requiring a rebuild (seals, bearings, slipper pads — approximately $400-600 in parts and labor). Over the truck's 15-year service life, the gear-pump approach requires 3-4 replacements ($900-2,400 total) versus one piston-pump rebuild ($400-600). The piston pump is the lower-cost option over the equipment life.
Q4: What causes the drum to slow down or stop under load — and is it always the pump?
Drum slowdown under load has three possible causes, and the pump is only one of them: (1) Pump internal leakage — worn piston slipper pads or port plate allowing oil to bypass internally. Diagnose by measuring case-drain flow: more than 10% of theoretical pump flow at maximum pressure indicates internal wear. (2) Hydraulic motor internal leakage — same failure mode but at the motor end of the circuit. Diagnose by measuring motor case-drain flow separately. (3) Relief valve cracking below set pressure — a fatigued relief-valve spring allows the valve to open at 200 bar instead of the specified 280 bar, dumping pump flow to tank. Diagnose by installing a pressure gauge at the pump outlet and observing the pressure at which drum rotation stops — if it stops at a consistent pressure below the relief-valve setting, the relief valve is the problem. In my experience, approximately 40% of "pump failure" diagnoses are actually relief-valve failures — replacing the pump does not fix the problem.
Q5: Is a pressure-compensated or load-sensing pump control strategy better for drum drive?
Pressure compensation maintains a constant system pressure by varying pump displacement — simple, reliable, and adequate for most drum-drive applications where the drum speed does not need to be precisely controlled. Load sensing maintains a constant pressure differential across a proportional directional valve by varying pump displacement, providing precise flow control independent of load — preferred for applications where drum speed must be held within 1-2 RPM regardless of concrete viscosity changes. The cost premium for load-sensing control is approximately $200-400 per pump. For standard transit mixers, pressure compensation is sufficient; for volumetric mixing trucks where precise water-cement ratio control requires precise drum-speed control during discharge, load sensing is the appropriate specification.
Q6: How does ambient temperature affect piston pump performance in mixer trucks operating in extreme climates?
In Arctic conditions (-40°C cold-soak), hydraulic oil viscosity can reach 5,000-10,000 cSt — 100-200 times the optimal operating viscosity of 30-50 cSt. Starting the pump under these conditions without preheating causes cavitation at the pump inlet because the oil cannot flow into the pump cylinders fast enough to fill them. The pump operates with partially filled cylinders, the pistons hammer against the swashplate on each stroke, and the slipper pads can fracture within minutes. The solution: an electric immersion heater in the reservoir (1-2 kW, thermostatically controlled to 20-30°C) that preheats the oil before engine start. In desert conditions (50°C ambient), the opposite problem occurs: oil viscosity drops to 10-15 cSt, reducing the lubricating film thickness at the slipper-pad/swashplate interface and accelerating wear. The solution: an oil cooler (air-to-oil or water-to-oil) sized to maintain oil temperature below 80°C at maximum ambient. Both the heater and cooler add cost but are mandatory for mixer trucks operating at temperature extremes.